All-Steel Antistatic Floor Manufacturer: What Sets the Best Apart
2026-09-03
When you're outfitting a data center or lab, the floor beneath your feet matters more than you think. All-steel antistatic flooring isn't just about durability—it's about precision, safety, and long-term reliability. But with so many manufacturers claiming excellence, how do you spot the one that truly delivers? At Lipin Floor, we believe the difference is in the details most suppliers overlook. This post unpacks the key factors that separate a genuinely superior all-steel antistatic floor from the rest—before you make a costly decision.
Steel That Holds Its Shape When the Room Gets Hot
Some metals go soft the moment things heat up, but this steel doesn't flinch. When temperatures climb high enough to make ordinary structural materials sag or creep, it locks its geometry in place—no warping, no slow bending under load. The secret lies in a carefully tuned alloy composition that resists thermal expansion and maintains yield strength far beyond what standard carbon steel can handle.
Engineers turn to this material for furnace components, exhaust systems, and high-temperature jigs where dimensional stability is non-negotiable. Even after repeated heating and cooling cycles, parts made from it keep their original tolerances, reducing maintenance downtime and scrap rates. That predictability means fewer surprises during production runs and less guesswork in design.
Compared to nickel-based superalloys, it offers a practical balance of cost and performance. You don't need cryogenic cooling or exotic coatings to make it work in demanding thermal environments. Just machine it, weld it, and let it sit in the heat—it will stay exactly where you put it.
Grounding Paths Checked at Every Joint
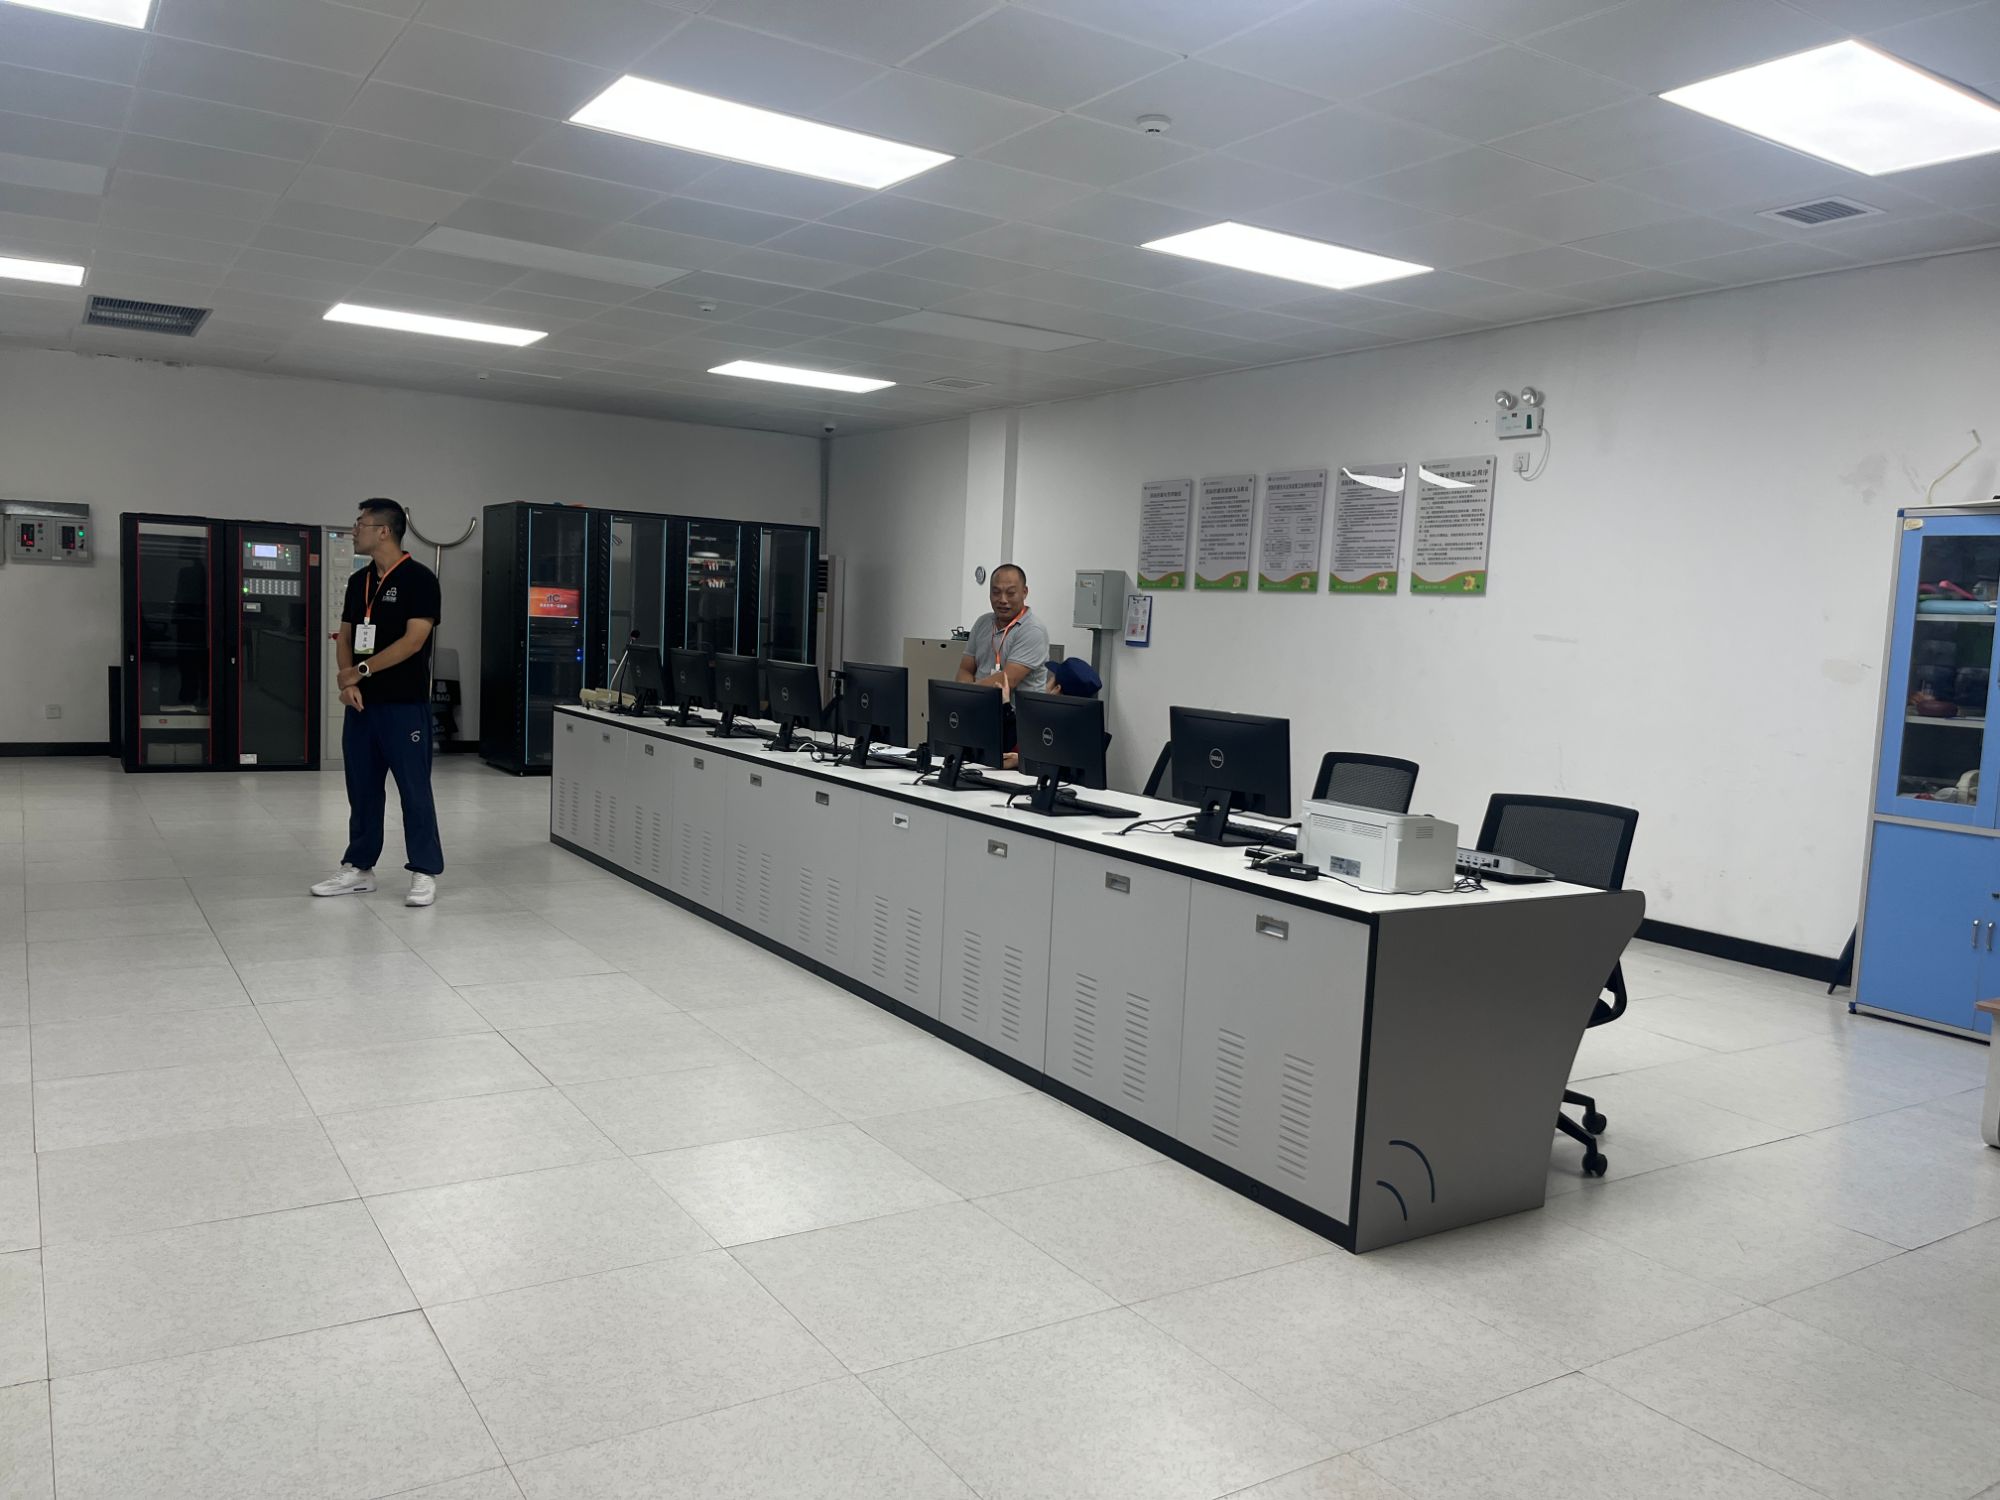
Each joint along a grounding path creates a potential failure point, so checking them individually requires more than just a quick visual sweep. A common practice begins with loosening and re-tightening mechanical lugs, splice bolts, and bonding jumpers to confirm they seat fully against the conductor or enclosure. Where conduit serves as the equipment grounding conductor, the locknut-to-enclosure interface and any eccentric or concentric knockouts need separate attention because paint, oxidation, or a slightly cocked ring can leave the path electrically open even when the assembly looks tight.
Field testing usually pairs a low-resistance ohmmeter with a known reference point, moving joint by joint rather than relying on one end-to-end reading. Values below one ohm are typical for short runs, but the trend matters more than the absolute number: a joint that measures noticeably higher than its neighbors often indicates a loose screw, a burr under a clamp, or a thin film of corrosion. In older installations, thermal imaging after load has been applied can also expose joints that pass a static resistance check but begin to degrade under current.
Documentation should record each checked joint, the tool used, and the measured value or pass/fail result, so future changes can be traced. If any joint fails, the repair usually involves cleaning the mating surfaces to bare metal, replacing pitted hardware, and retorquing to the manufacturer's specification rather than simply cranking the fastener harder. This joint-by-joint discipline keeps the overall grounding path dependable without assuming continuity through painted enclosures or weathered fittings.
The Difference Between a Coating and a Bond
A coating is essentially a surface layer applied to a substrate, primarily to protect, decorate, or add specific functionality. It does not require chemical bonding with the underlying material; instead, it relies on physical adhesion or mechanical interlocking to stay in place. Think of a coating as a jacket worn over clothing—it covers and shields, but it can be removed without destroying the garment underneath. In contrast, a bond refers to a strong connection formed between two materials, often involving molecular forces, chemical reactions, or metallurgical fusion, making the interface extremely difficult to separate. Here, the materials become one unit, like two pieces of metal welded together.
The key difference lies in the nature of the interface. A coating usually has a distinct boundary that remains visible under magnification, and it may peel or delaminate under stress, corrosion, or thermal cycling. A well-formed bond, however, often creates a diffuse or blurred interface—sometimes even a transition zone—which allows the joint to transfer loads effectively. In practical engineering, coatings are selected for their surface properties such as wear resistance, corrosion protection, or low friction, while bonds are chosen for structural integrity, as seen in adhesive joining, brazing, or thermal spray coatings that achieve metallurgical bonding. This distinction guides decision-making in surface treatment and joining technologies.
Why Not All Load Ratings Survive the First Roll
That load rating printed on the tire sidewall looks like a hard number, but it's actually a lab result frozen in time. Real pavement has no interest in lab conditions. The first roll drags that rating through heat, side loads, and the sudden violence of a pothole or highway seam. A tire can carry its rated load on a smooth drum for hours, then tear a belt on its first real corner because the rating never accounted for lateral scrub. If the wheel is slightly out of round or the inflation is five psi low, the load sits differently, and the safety margin shrinks fast.
Some ratings survive because the maker left extra material in the sidewall or used a tougher bead compound. Others are optimistic stamps pushed to the edge of the material's fatigue curve. First roll is when those truths surface. Rubber that heats up past its design window stops bouncing back. A bead that creeps under load loses its seat. Even two tires from the same mold can diverge once real cargo shifts and curb strikes happen. The rating that survives is always the one with a hidden cushion, not the one that looked strongest on paper.
Built for the Spec You Actually Have, Not the One in the Brochure
Most tools optimize for a lab environment or a top-tier review unit, then fall apart on the mid-range laptop sitting on your desk. This one flips that logic. It reads the actual hardware you're running—RAM, storage speed, thermal limits—and adjusts its behavior to match. No background processes fighting for memory you don't have. No features silently disabled because the CPU isn't on some approved list. You get the full experience scaled to what's really there, rather than a stripped-down version waiting for an upgrade you may never make.
The result is less time staring at loading screens and more time doing the work. On a machine with integrated graphics and 8GB of RAM, it stays snappy by keeping the interface lightweight and prioritizing active tasks. On a high-end workstation, it stretches out and uses every core you paid for. The brochure numbers stop mattering because the tool respects the machine in front of you, not the one in the product photos.
When the Install Team Leaves, the Real Test Begins
A smooth handover creates a dangerous illusion. Once the installers pack their tools and drive off, the polished surfaces and neatly routed cables suggest the hard part is over. In practice, this is when the system first meets the messy reality of daily use. Users click things nobody trained them to avoid. Power fluctuates. Network conditions shift. The real test isn't whether the equipment powers on, but whether it still feels reliable at 3 p.m. on a Thursday, three weeks after the van disappeared.
Most failures surface during those early unsupervised days. A sensor drifts out of calibration. A backup silently skips a schedule. Someone plugs a space heater into the wrong circuit and nobody notices until the logs fill with voltage warnings. The installers were focused on getting from zero to operational; the long-term question is whether the setup can degrade gracefully without constant hand-holding. That gap between what the documentation claims and what actually happens is where trust either forms or quietly dies.
Treat the departure of the install team as day one, not the finish line. Watch the first two weeks of routine operation with the same attention you gave the commissioning checklist. Note the small annoyances, the error messages no one expected, the workaround someone invented on the fly. Those details tell you more about the system's true health than any acceptance sign-off. If you only test while the experts are still in the building, you haven't tested your operation—you've tested their preparation.
FAQ
All-steel panels handle heavy rolling loads without flexing or cracking the way composite panels sometimes do. Their conductivity doesn't rely on a surface film that can wear away, so the grounding path stays consistent for years.
The gap shows up in edge finishing, weld quality, and how tightly the panels fit the pedestal heads. A top manufacturer also runs batch-level electrical tests and clearly documents the results instead of pointing to a single outdated sample.
Check whether the conductivity is built into the steel or comes from a permanent copper strip under the panel. Ask for recent third-party resistance reports tied to actual production lots, not just marketing claims.
It often is. The best suppliers can adjust panel dimensions, add cable cutouts, or match non-standard pedestal heights without delaying the project. That kind of flexibility reduces risky field modifications that can break the grounding path.
Look for at least 10 years on structural performance and 5 years on antistatic properties. Insist on written terms that define what actions void the coverage—vague verbal assurances are a red flag.
They do. Higher-end manufacturers machine pedestal heads for a snug panel fit and coat stringers to resist corrosion. Low-cost alternatives often wobble under load and lose conductivity at the joints.
Ask whether they test every batch for surface and point-to-point resistance plus load deflection. Reliable manufacturers will share their testing setup and provide certificates with serial numbers that match your delivered panels.
Conclusion
The best all-steel antistatic floor manufacturers don't lean on a single selling point. They start with steel that holds its shape when the room gets hot, because thermal expansion is exactly where cheaper panels start to buckle or show gaps. Grounding paths get checked at every joint, not just the ones you can see; one loose connection turns the whole floor into a static trap. And the difference between a coating and a bond is not cosmetic. A coating can peel, chip, or wear away, but a true bond becomes part of the steel itself, keeping conductivity steady under rolling chairs and daily foot traffic.
Load ratings look great on a datasheet until the first roll test sends a loaded cart across the panel. The manufacturers worth keeping design for the spec you actually have, not the one in the brochure, which means asking about point loads, vibration, and real traffic patterns before cutting a single sheet. When the install team leaves, the real test begins. Panels shouldn't creak, shift, or lose their grounding path after a month of use. A lot of floors pass the walkthrough on day one and start failing by week three. The best manufacturers stand behind that longer stretch, not just the handover handshake.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/