Laser Safety Apron Factory: Ensuring Optimal Protection for Your Team
2026-10-06
Every day, your team works in environments where invisible laser hazards can cause irreversible harm in a split second. Choosing the right protective gear isn't just about compliance—it's about keeping the people behind the work safe. At LASERPAIR, we don't just manufacture laser safety aprons; we engineer confidence into every layer, so your crew can focus on precision without second-guessing their protection. Here's what makes our factory different.
Beyond Standard Aprons: What Actually Stops a Laser Beam
Standard aprons, the ones you find in most workshops or labs, are little more than fabric placeholders when a laser is involved. A 5-watt diode laser will chew through denim or canvas in under a second, and the cotton-poly blends commonly used for splash protection offer zero resistance to focused light. What actually stops a beam isn't thickness or toughness in the traditional sense—it's optical density and thermal stability. Materials like anodized aluminum, certain borosilicate glasses, or specialized polymer composites are engineered to absorb or reflect specific wavelengths, turning a potential burn into nothing more than a warm spot.
The key isn't just blocking the light; it's handling the heat that comes with it. A piece of steel might reflect a visible laser, but the same beam in the infrared range can heat the metal fast enough to cause secondary burns or start a fire. That's why effective laser barriers are wavelength-matched. For example, a ruby-red acrylic shield that stops a 445nm blue laser brilliantly may be nearly transparent to a 1064nm fiber laser. Without that match, you're essentially wearing a mirror or a window—one that gives a false sense of safety while the beam does its work.
So before you trust any apron, check the optical density rating—usually expressed as OD, like OD 4+ or OD 6+—and the specific wavelength range it covers. A true laser apron won't be floppy or fabric-like; it'll have a rigid or semi-rigid front panel, often with a matte finish to diffuse stray reflections. And remember: side and back exposure matter too. A laser bouncing off a metallic clamp or a glass beaker can hit you from an angle no front-facing panel will cover. Stopping a beam is less about wearing armor and more about engineering the entire workspace so the beam never reaches your skin in the first place.
The Hidden Costs of Skipping Proper Laser PPE
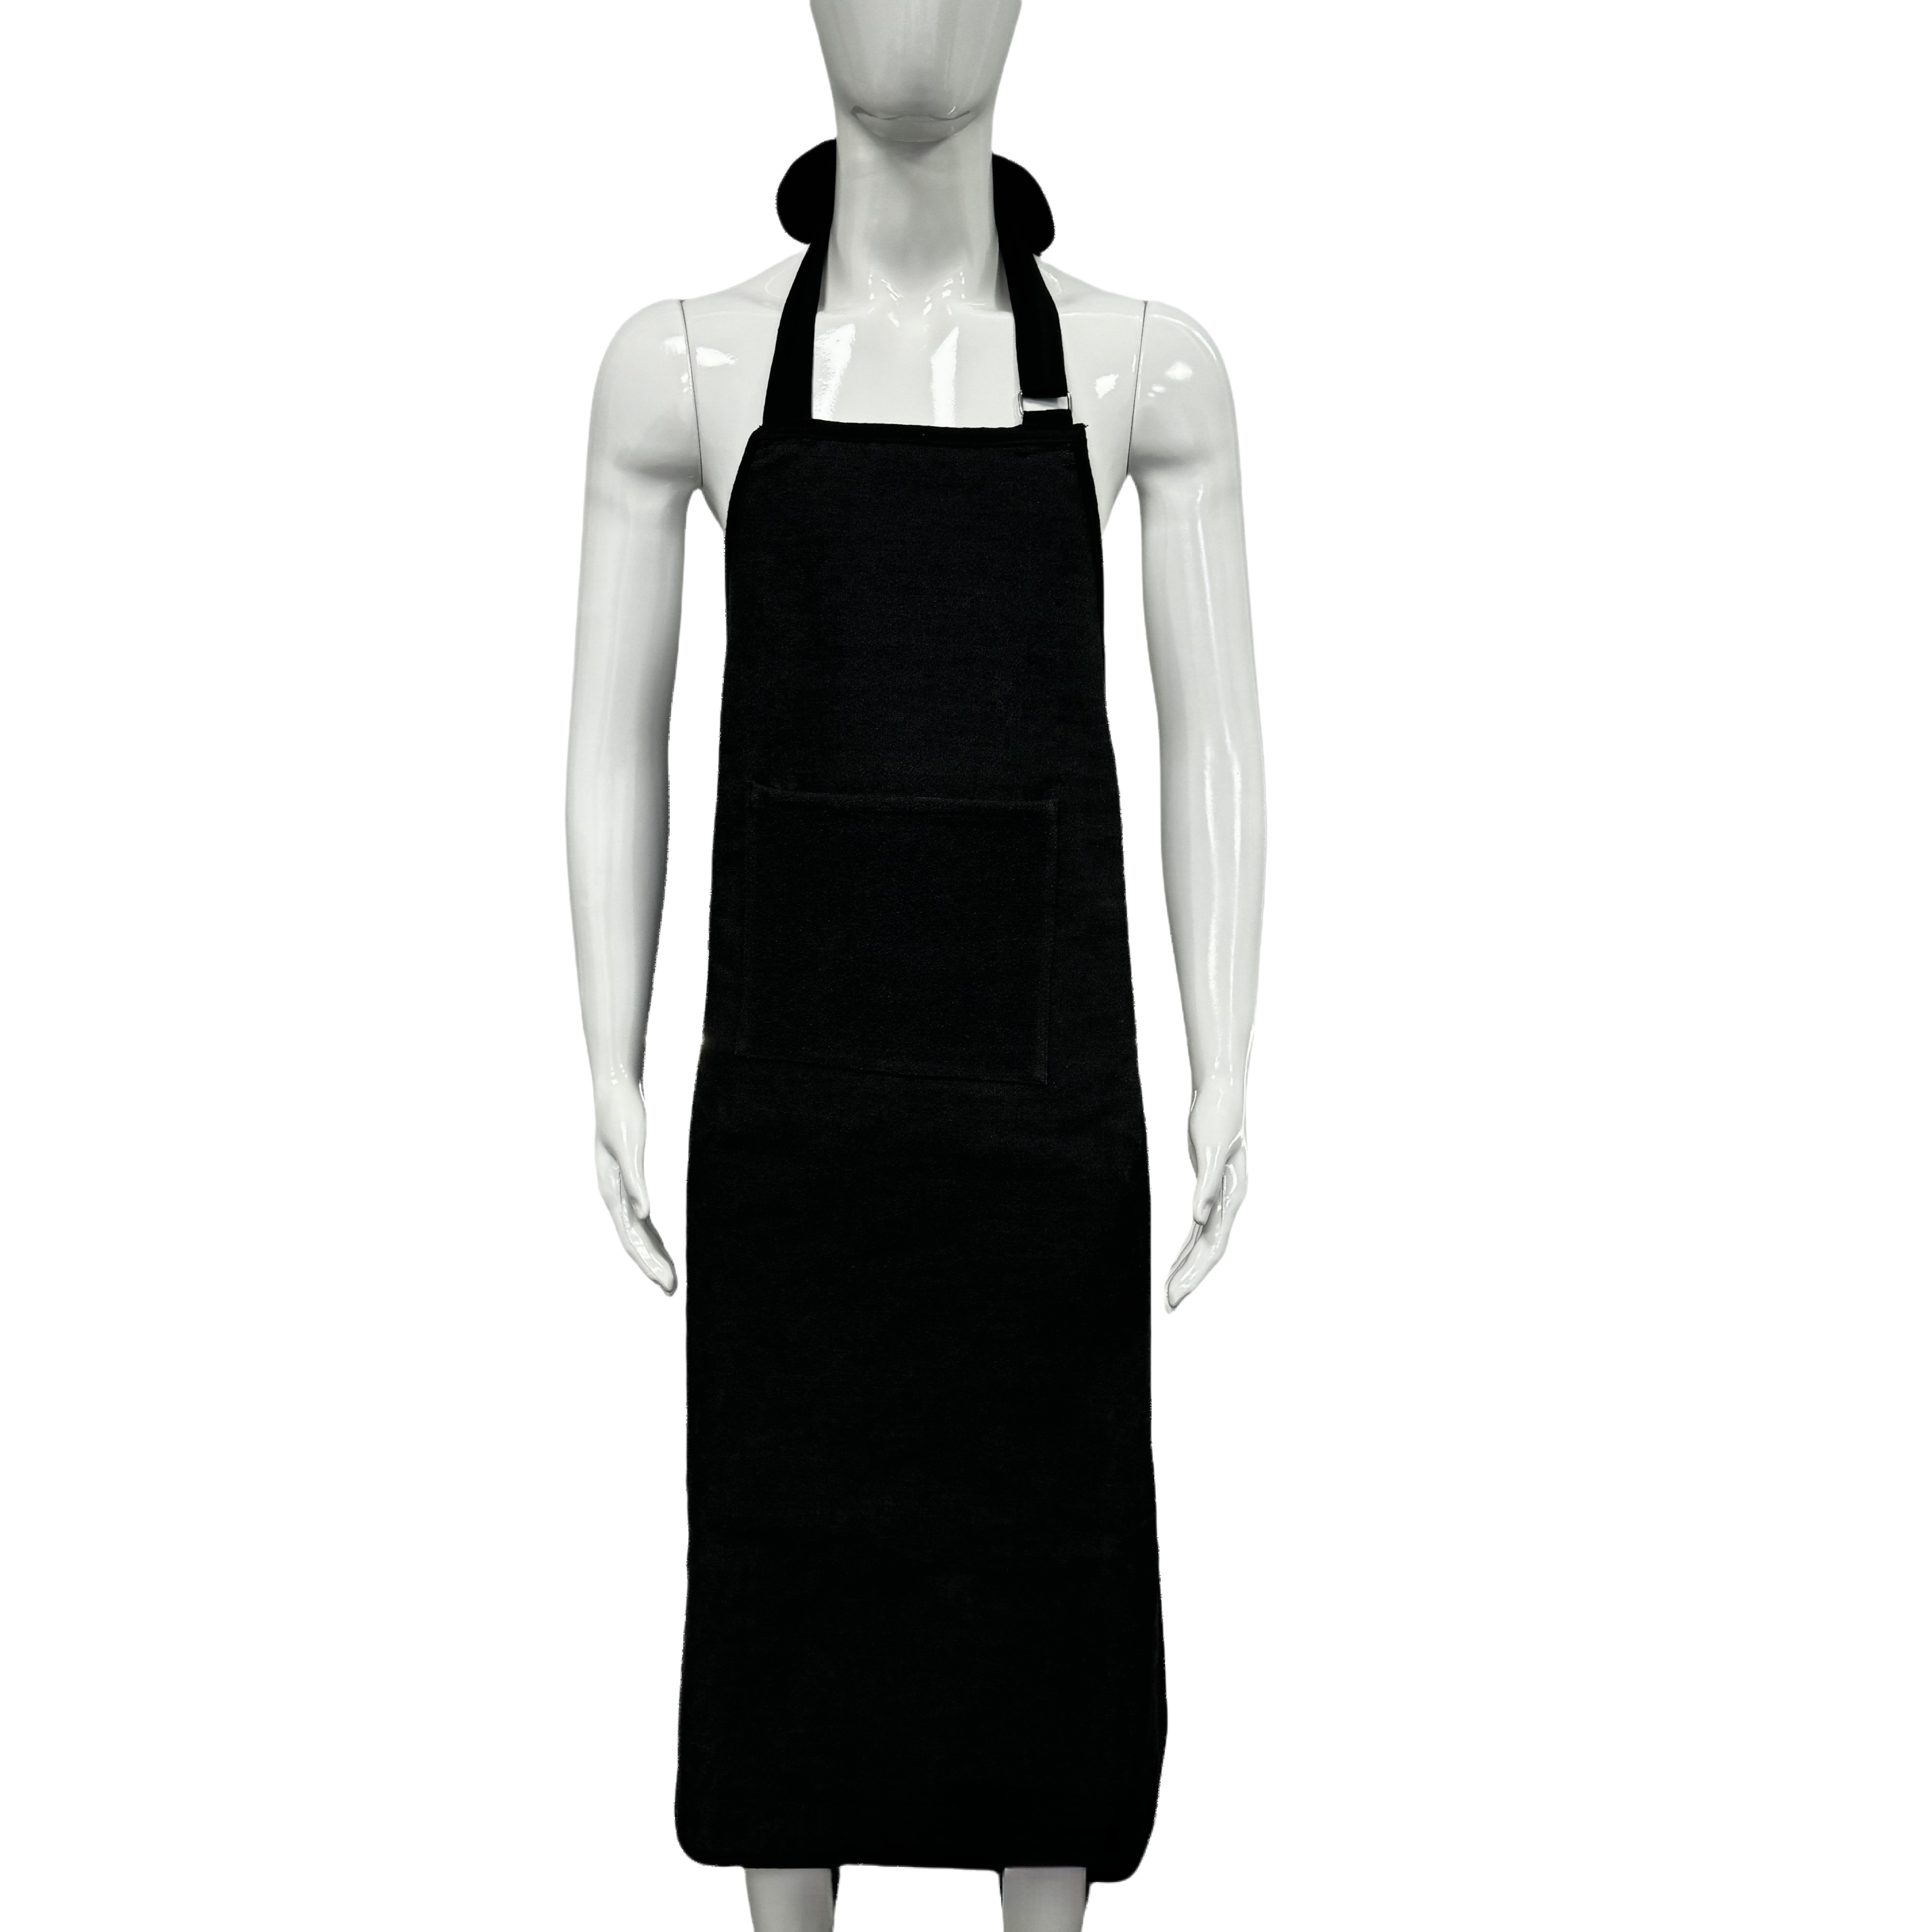
Operators often treat laser safety glasses as an optional accessory when the beam power seems low or the exposure time feels brief. A quick alignment task, a brief reflection check, or a momentary glance at a diffuse spot can slip by without proper eyewear. Yet retinal tissue has no pain receptors, so damage registers silently. Single-pulse exposure from common industrial lasers can permanently scar the macula, and scattered light from class 4 systems remains hazardous meters away. Replacing a pair of certified goggles costs far less than a lifetime of degraded central vision or a worker’s compensation claim tied to avoidable ocular trauma.
The financial and operational burden goes beyond medical bills. Downtime from an incident triggers mandatory investigations, retraining, and possible regulatory fines. Team productivity stalls while equipment sits idle, and morale drops when colleagues realize the injury was preventable. Insurance premiums climb after a reportable laser injury, and credibility with clients or institutional review boards can erode. Many facilities discover that the true price of skipped PPE is not just the goggles they failed to buy, but the compounding cost of a safety culture failure that takes quarters to repair.
Choosing the right laser PPE also matters for task efficiency. Mislabeled or generic eyewear can block the wrong wavelengths, leaving workers falsely confident while exposed. Conversely, badly matched filters darken the field unnecessarily, forcing risky removal mid-task. Proper protection lets technicians maintain visual confirmation of beam positions without hesitation, reducing errors and rework. When laser safety glasses are treated as precision tools rather than bureaucratic checkboxes, the hidden costs of shortcut-taking disappear from both the balance sheet and the team’s long-term health.
How Our Factory Tests Every Apron for Real-World Hits
We don't just toss a finished apron into a box and call it done. Every batch gets pulled at random and run through a gauntlet that mimics the dumb accidents of a busy shift: hot oil spatter, a full coffee mug knocked across the front, a snag on a drawer handle mid-stride. If the fabric shows wear before the test ends, the whole batch is held back.
The stress points get more attention than the pretty parts. We fold, yank, and twist the neck straps and waist ties the same way a line cook does when they're in a rush. Stitching is checked under a light for skipped threads, then the seams are stretched against a weight bench until the thread gives or the fabric rips. We'd rather destroy aprons here than have one fail on someone during dinner service.
Real hits also mean real washing. Aprons go through repeated hot-water cycles with the same industrial detergents used in restaurant laundries, then get yanked out and inspected while still damp. Shrinkage is measured, stains are left to sit overnight, and pockets are stuffed with heavy spoons and thermometers to see if they sag. Only after that does a style get the green light to ship.
Comfort Meets Compliance: Designing for All-Day Wear
Achieving true all-day comfort in regulated footwear means refusing to treat compliance as an afterthought. The pinch points that irritate by hour three often come from stiff toe caps or unyielding midsoles, so our design process starts with pressure-mapping data and real wear trials rather than just checklist specs. We adjust collar padding, heel counters, and lace tension zones until the shoe disappears on the foot, even after a ten-hour shift or a long factory floor walkthrough.
Compliance remains non-negotiable, but it doesn't have to announce itself with every step. We use lower-density polyurethane foams and breathable mesh linings that meet ASTM or EN standards without adding bulk. Each round of prototyping includes subjective feedback from nurses, warehouse crews, and lab technicians who log 20,000+ steps daily. Their blister reports and end-of-day fatigue scores shape the next iteration, so the final design earns its safety rating and still feels like a shoe you'd choose on a day off.
Why Material Thickness Alone Won't Save Your Team
It's easy to assume that beefing up material thickness will solve your structural problems, but that mindset rarely holds up in real-world design. Teams often reach for thicker plates or heavier gauge steel as a quick fix, only to discover that the core issue lives elsewhere—whether in load paths, joint design, or manufacturing tolerances. Thickness can mask a symptom, but it won't address the root cause.
Adding material thickness introduces a cascade of trade-offs that can quietly undermine a project. Extra weight drives up cost, complicates assembly, and may even reduce performance in dynamic applications. A thicker part can create stress concentrations at connections or alter the balance of a system, forcing the team to chase new problems downstream. Without careful analysis, you're simply trading one failure mode for another.
What actually saves a team is a willingness to question assumptions and collaborate across disciplines. Engineers, fabricators, and end users each bring insights that no single parameter can replace. By simulating loads, prototyping iteratively, and sharing feedback early, a group can optimize geometry, material selection, and process—turning thickness into just one tool among many rather than a crutch.
Built Like Armor, Worn Like Workwear: The Factory Difference
Plenty of brands claim toughness; few spend time in a cutting room watching fabric get dragged across concrete. The first thing you notice with this line is the weight. It’s not the dead weight of a denim jacket. It’s a dense, almost leather-like hand that comes from a 12-ounce duck canvas we had milled to a tighter weave than standard workwear. That means you can kneel on rough asphalt or brush against a metal edge without that immediate cringe. The fabric takes the hit, not your skin.
The factory difference really shows up in the small decisions. Every seam that carries load—shoulder, side, crotch gusset—gets a double needle with a slightly longer stitch length. That’s not an accident. Shorter stitches punch too many holes and weaken the cloth. Longer stitches let the panel flex. It’s the kind of detail you only find when the person running the line has been doing it for twenty years and refuses to cut corners even when nobody’s watching.
Then there’s the fit. Workwear shouldn’t fight you. We cut the sleeves a touch higher under the arm so you can reach a top shelf without the whole jacket pulling up. The collar is softer than it looks, shaped to lie flat under a tool belt or a backpack strap. It’s built like armor in the places that matter, but it wears like a shirt you’ve had for years—because that’s the only way workwear should feel at the end of a long shift.
FAQ
Laser aprons have to handle concentrated beams, not just sparks and splatter. We layer a specialized reflective outer shell over a dense, heat-resistant core so the energy disperses rather than burning through. Welding gear doesn't have that kind of optical density rating.
Our standard range covers Class 3B and Class 4 lasers, though we can build for lower classes too. The protective rating is tied to wavelength and exposure time, so we'd ask about your specific setup before recommending a fabric weight.
Yes, we offer a full size run from small to 4XL, and we can adjust strap lengths, chest width, and length at no extra cost. For unusual body types or mobility requirements, send a few measurements and we'll pattern it individually.
It depends on the laser power and how often it's hit directly. Under normal indirect exposure, most teams get two to three years. Direct beam contact will degrade the outer layer faster, so we recommend an inspection every six months and replacement if you see surface cracking or discoloration.
Each production lot is tested against EN 60825-4 for laser protective eyewear and apparel, and we also align with ANSI Z136.7 for laser safety equipment. We can provide a certificate of conformity with your order if your safety auditor needs it.
We don't patch laser aprons because any seam or added layer can become a weak point. Instead, we offer a trade-in discount when you send back worn aprons, and we recycle the metalized fabric. It keeps your team protected and your costs down.
A full apron gives coverage to the knees and is better for bench work or standing at a laser table. A vest is lighter and works when you need more arm mobility or you're moving between stations. We can also build a split-leg apron if you need to sit or crouch.
Standard sizes usually ship within two weeks for orders up to 50 units. Custom sizing or special fabric requests add about a week. If you need a rush order, we can often split the shipment and send the most critical sizes first.
Conclusion
A laser apron that merely looks thick often fails under real beam exposure, which is why this factory goes beyond standardized material specs. Instead of relying on thickness alone, each apron is built from specialized layered composites that absorb and dissipate specific wavelengths, tested repeatedly against direct hits and angled strikes. The testing protocol simulates real workshop conditions—not just lab certifications—so every unit that leaves the floor has survived impacts that would compromise ordinary protective gear. Meanwhile, the design team works to ensure the apron remains wearable for full shifts, balancing weight distribution and flexibility so compliance doesn't come at the cost of mobility or endurance. Skipping proper laser PPE carries hidden expenses: injuries, downtime, regulatory fines, and eroded team trust, all of which dwarf the upfront investment in certified protection.
What sets this factory apart is the fusion of armor-grade defense with practical workwear ergonomics. Rather than treating protection as a rigid afterthought, the manufacturing process treats the apron as daily equipment—adjustable straps, breathable backing, and reinforced stress points that maintain integrity after months of use. Unlike generic vendors who push thicker panels as a false solution, the factory engineers each layer for a specific role: reflection, absorption, and thermal dispersion. The result is a garment that stops laser energy like dedicated armor but feels familiar enough to be thrown on without hesitation at the start of a shift. This approach closes the gap between written safety standards and genuine on-the-job resilience, giving your team confidence that the protection they wear has already proven itself under fire.
Contact Us
Contact Person: Jenny
Email: [email protected]
Tel/WhatsApp: +86 13537713281
Website: https://www.laserpair-safety.com/