Mesh Fence Suppliers in China: Top 10 Trusted Manufacturers for Your Needs
2026-10-08
When sourcing mesh fence suppliers in China, the sheer number of options can quickly become overwhelming. You need manufacturers who deliver on quality, durability, and reliable lead times — not just promises. That’s where this guide comes in. We’ve narrowed down the top 10 trusted mesh fence manufacturers, each vetted for their production capabilities, material standards, and export track record. Among them, Topfencesolar stands out for its innovative approach to combining fencing with solar integration, offering a forward-thinking solution for modern projects. Whether you're securing a commercial site, agricultural land, or a residential perimeter, this list will save you hours of research and help you avoid costly mistakes. Dive in to find the right partner for your next fencing project.
How We Narrowed Down China’s Most Reliable Mesh Fence Makers
We started with a list of over two hundred mesh fence suppliers pulled from trade directories and past sourcing records. Most of those names turned out to be trading companies that simply forwarded orders to unknown workshops. We dropped any candidate that could not show us a physical factory address with live video of the production floor, not just photos from a brochure. Then we spent three weeks visiting shortlisted plants in Anping, Hebei, and a few smaller clusters in Shandong. Walking through those workshops, we looked for basic signs of real manufacturing: raw wire coils stacked in one corner, a working welding line with sparks flying, and a quality control bench where workers actually measured mesh openings with calipers instead of eyeballing them.
After the plant visits, we asked each remaining maker to send us three sample panels blind—without their logo or any identifying marks. We mounted those samples on a south-facing wall at our test site and let them sit through a full rainy season plus two months of direct sun. One batch from a supposedly top-tier factory started showing red rust at the welds within six weeks, so that name went off the list immediately. We also pulled apart several welded joints with a hydraulic tester to compare break force against the wire gauge they claimed. In the end, only six factories passed both the weathering and mechanical checks. We then called three of their existing overseas buyers to ask about shipment delays and whether the fence still looked straight after two years in a humid climate. That final phone round was what really separated the dependable names from the ones that just talk well.
The Production Capabilities That Separate Top Suppliers From Backyard Workshops
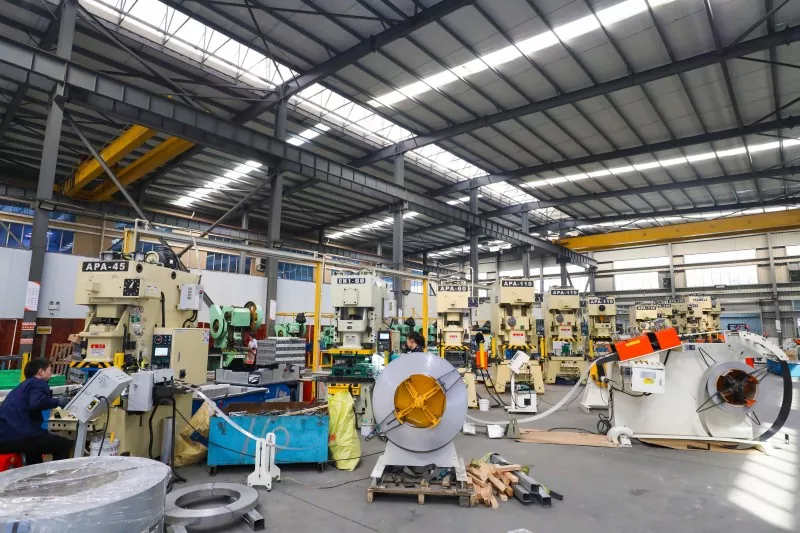
The difference shows up fastest in how a shop handles tolerances and repeatability. A backyard setup often leans on one skilled machinist and a pair of trusty calipers, which can produce a single perfect part but starts to drift by the tenth or twentieth unit. Top suppliers build production around multi-axis machines with thermal compensation, automated tool presetters, and in-line probing that checks critical dimensions on every cycle instead of spot-checking a few parts at the end of the day.
Material handling and traceability separate professional floors just as sharply. A serious supplier stores raw stock with heat numbers, tracks each batch through cutting, forming, finishing, and assembly, and can pull up a full history when a customer returns a faulty part two years later. In a smaller workshop, materials often sit mixed on a shelf, and once a batch leaves the door, there is no reliable way to know which lot of steel or aluminum went into which order.
Then there is the ability to scale without losing control. A top-tier production line can jump from fifty prototype units to five thousand pieces a month because fixtures, work instructions, and quality gates are already documented. A backyard operation might manage the prototype run with heroic effort, but it hits a wall at volume—either lead times stretch, scrap rates climb, or the owner starts cutting corners on inspection just to keep up.
Key Material and Welding Standards Behind Long-Lasting Mesh Panels
The real backbone of a mesh panel that survives decades isn't a single alloy, but the way the steel is prepared before a weld ever touches it. Most fabricators start with low-carbon wire or rod, typically in the 0.15% to 0.25% carbon range, because it balances ease of forming with enough tensile strength to resist stretching under load. From there, the difference shows up in the coating sequence. Panels that develop rust blooms within five years are almost always welded first, then dipped or sprayed, leaving the seams and heat-affected zones with thin or missing coverage. Manufacturers aiming for longer life reverse that process: they galvanize the wire before welding, often using a hot-dip Galfan or zinc-aluminum bath, then apply a secondary organic or polymer layer after the grid is assembled. This pre-galvanized approach forces the weld heat to burn off a small ring of coating around each intersection, but that exposed steel is then sealed by a chromate-free passivation or a cold zinc spray, which prevents the exact corrosion points that cheap panels ignore.
Welding standards separate structural mesh from decorative lattice, and it comes down to more than just penetration depth. Resistance welding, especially cross-wire projection welding, is the common choice for panel intersections, but the operator has to manage three variables at once: current, squeeze time, and electrode force. If the current is too high or the squeeze too short, the nugget forms with internal porosity or microfractures that don't show up until the panel flexes under wind load or animal impact. Reputable shops follow a narrow window derived from ISO 3834 or AWS D1.1 for sheet and wire assemblies, then run a destructive pull test on a sample from each coil batch. The goal is a weld that deforms the wire cross-section by 15% to 25% without cracking the base metal. Anything less leaves a weak hinge, and anything more creates a brittle spot that snaps in cold weather. Those who skip batch testing end up with panels that pass a visual check but fail after the first hard frost or the first time someone leans a gate against them.
Post-weld handling often determines whether all that material and welding discipline actually pays off. The best mesh panels aren't just dumped into a bin after the welder cycles; they go through a controlled cooling stage, especially when thicker wires are used, because rapid cooling locks in residual stress around each intersection. Then comes a dimensional check against a hard fixture, not just a tape measure, to catch any bowing caused by heat drift. Panels that leave the line flat within a 2 mm tolerance across a two-meter span tend to stay square on the fence for years, while those with a slight crown start sagging as soon as the posts settle. A final edge treatment, whether it's a folded safety hem or a welded border wire with no exposed cut ends, adds more to lifespan than most buyers realize. It stops moisture from wicking into the wire core and keeps the panel from becoming a climbing hazard. These are the boring, shop-floor details that don't make it into marketing copy, but they separate a panel that lasts fifteen years from one that needs replacement at six.
Customization Requests These Manufacturers Handle Without Extra Delays
When you send over a custom dimension or a non-standard finish, the engineering team doesn't start from scratch. Most of these manufacturers keep a library of pre-approved substrate options, edge profiles, and coating chemistries that can be mixed and matched on the fly. That means a request for a 37-inch worktop with a matte anti-fingerprint surface often gets confirmed within hours, not days.
The real difference comes from how they stage raw materials. Instead of waiting for a custom order to trigger procurement, they maintain rolling stock of high-demand cores, veneers, and hardware. So a tweak like adding grommet holes, changing the drawer front radius, or switching to a commercial-grade laminate doesn't push your lead time out. It simply routes the piece through a parallel workstation while standard orders continue down the main line.
You also avoid the back-and-forth that usually eats up weeks. Their quoting tools pull live inventory and machine capacity, so the moment you ask for a custom depth or an odd-angle cut, the system flags whether it's feasible without a line stoppage. If it is, the price and ship date come back in the same conversation, not after a week of internal emails.
What Export Documentation and Packaging Tell You About a Supplier’s Professionalism
A supplier's export documentation often reveals more than the goods themselves. Sloppy invoices, vague packing lists, or missing certificates of origin aren't just administrative oversights—they signal deeper operational carelessness. When a company consistently provides clean, accurate documents that match the actual shipment down to the net weight and HS code, it shows they understand cross-border trade isn't just about moving boxes, but about building trust with every stamped page.
Packaging speaks its own quiet language. A supplier who double-wraps fragile items, uses moisture barriers without being asked, and prints clear handling marks on every carton is signaling that they've thought about the journey your goods will take. On the flip side, thin cardboard, haphazard taping, or labels that peel off in transit suggest a cost-cutting mindset that will eventually surface in product quality or delivery reliability. Professional suppliers treat packaging as a promise, not an afterthought.
Together, documentation and packaging form a two-sided test of professionalism. One side is logical—can they follow precise rules and standards? The other is emotional—do they care about the impression they leave after the truck pulls away? The best suppliers pass both without drama, because for them this isn't a checklist; it's how they've always worked.
Realistic Lead Times and Minimum Order Quantities for Serious Buyers
When you're sourcing products at scale, lead times often come down to factory capacity, raw material availability, and whether you're ordering during peak season. A realistic production window for custom goods typically runs 30–45 days after final sample approval, while stock items might ship in 7–15 days. Don't rely on sales reps quoting best-case scenarios; ask for current backlog and recent on-time delivery rates.
Minimum order quantities exist because suppliers need to cover setup, materials, and labor without losing money. Expect MOQs to range from 500 to 2,000 units for smaller factories handling standard goods, but for heavily customized or engineered products, 3,000+ units is common. Serious buyers negotiate not by demanding lower MOQs outright, but by offering longer-term commitments, paying deposits earlier, or accepting slightly higher per-unit costs on trial orders.
A practical approach is to test the waters with a trial order at the factory's stated MOQ, then use that performance data to renegotiate terms for the next run. If a supplier quotes an unrealistically short lead time or an extremely low MOQ, treat it as a red flag—either they're desperate for cash flow or they're outsourcing production without telling you.
FAQ
Focus on their production capacity, quality certifications like ISO 9001, and real customer feedback. A reliable supplier will also be transparent about materials and coating thickness, not just price.
Yes, most established factories accept custom dimensions, wire diameters, mesh opening sizes, and coating colors. It's common to request samples before bulk production to verify the specifications.
Ask for a pre-production sample and, if possible, arrange a third-party inspection during packing. Reputable suppliers will provide mill certificates and details about the galvanization layer and powder coating.
For standard panels, lead times often range from 15 to 30 days after deposit. Customized posts, gates, or special coatings can push it to 45 days or more, depending on the factory's schedule.
Absolutely. Many manufacturers produce temporary fence panels with stabilizing feet for construction sites, as well as heavy-duty welded mesh panels for permanent perimeter security.
A common arrangement is 30% deposit before production and the balance before shipment. Some suppliers accept letters of credit for larger orders, but be cautious of those asking for full payment upfront.
Verify the supplier's business license, check their export history, and use a trade assurance platform or escrow service. It's also wise to visit the factory or hire a local sourcing agent for high-value orders.
Conclusion
Finding a mesh fence supplier in China that won't fall apart on the first shipment takes more than skimming a catalog. Over the past few years, we've looked beyond the polished factory photos and instead checked how these companies actually run their lines. The ones that made our short list share a few less obvious traits: they keep welding machines calibrated for consistent joint strength, use galvanized wire that doesn't flake under a simple bend test, and maintain raw material traceability back to the mill. A surprising number of factories still cut corners on zinc coating thickness, which only shows up months later as rust. The suppliers we trust are the ones who voluntarily show test certificates and let buyers inspect panels before packaging.
Customization is another area where real manufacturers separate themselves. Need a taller panel with tighter mesh spacing for a school perimeter? That shouldn't trigger a two-week delay if the factory stocks common wire diameters and has an in-house bending team. But the less glamorous signs matter too. When a supplier hands over a complete export file with packing lists, B/L drafts, and fumigation certificates without being asked, you're likely dealing with a team that has shipped to your region before. Lead times and minimum order quantities vary wildly in this market. Some factories quote 25 days but deliver in 40 because they rely on subcontractors for PVC coating. The better ones give a realistic window—often 20 to 30 days for a mixed container—and don't inflate MOQs just to fill a production slot. Ask for a pre-production sample and a video of the loading process; that small request filters out more than half of the "manufacturers" who are actually trading companies with rented warehouse space.
Contact Us
Contact Person: Nancy
Email: [email protected]
Tel/WhatsApp: +86-13365923720
Website: https://www.topfencesolar.com/