OEM Rotary Dip Switches Factory Crafting Precision Components for Global Brands
2026-10-25
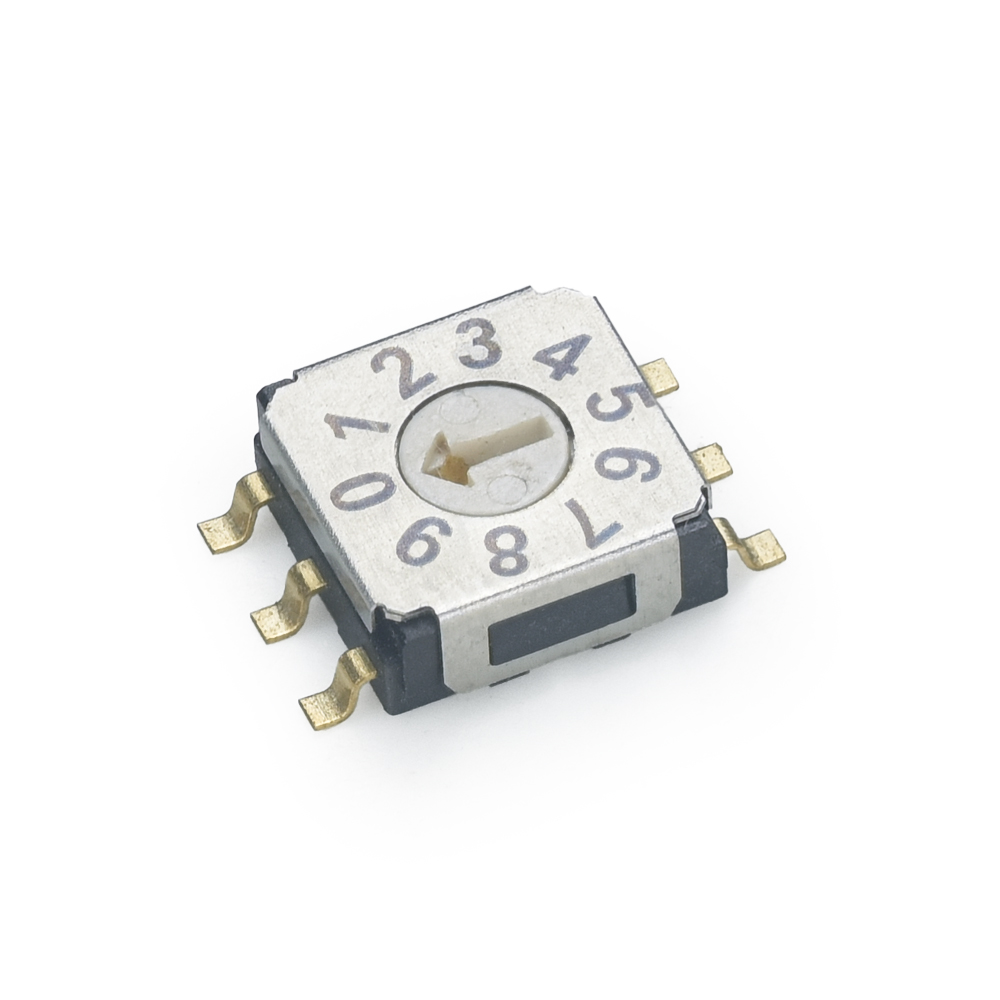
Behind every reliable electronic device lies a tiny yet critical component—the rotary dip switch. For global brands that demand precision without compromise, finding the right OEM manufacturing partner is everything. That’s where KEJIAN ELECTRONICS comes in, crafting rotary dip switches with tolerances measured in microns and consistency proven across millions of cycles. In this post, we’ll pull back the curtain on what separates a true precision factory from the rest—and why your next project might depend on it.
The Calibration Room Where Every Click Is Measured
Step inside and the first thing you notice is the hush—no random chatter, just the soft, deliberate tap of fingers on switches. Every press lands on a sensor bed that records force, dwell time, and micro-adjustments in posture. The room was built for one purpose: to strip away guesswork and turn each interaction into a clean data point. There’s no such thing as an idle click here; even the hesitant half-press before a full commit tells its own story.
Over by the far wall, a bank of monitors charts live curves for actuation distance and rebound speed. Engineers watch the traces drift across the screen, occasionally pausing to re-run a sequence with a different grip angle. The comparison isn’t about finding a “perfect” number—it’s about mapping how small changes ripple through hand fatigue and reaction time. A ten-gram difference in spring weight, invisible to the naked eye, produces a signature shift that only this room can capture.
What keeps people coming back is the feedback loop. You adjust a mechanism, click through a controlled set, and within minutes you’re looking at a normalized graph that shows exactly where your assumption broke down. No marketing gloss, no vague promises—just measured behavior under repeatable conditions. For anyone who has ever wondered why a button feels right or wrong, this room answers the question in hard numbers.
Mixing Custom Actuators With Off-the-Shelf Housings
Blending a custom actuator into an off-the-shelf housing rarely goes as smoothly as the datasheets suggest. The housing was never designed around your specific motor geometry, lead screw length, or sensor placement, so expect to spend time on adapter plates and cable routing. The upside is real, though: you keep the rugged, tested enclosure while getting exactly the force and stroke your application demands. Just don't assume the mounting holes will line up—verify every interface before committing to a batch.
Thermal behavior is another thing that catches people off guard. A sealed, off-the-shelf housing intended for a standard actuator might trap heat when you drop in a custom unit that runs hotter or has different duty cycles. If possible, run a short thermal test with the actual load and look for hot spots near the motor flange or gearbox. Sometimes a simple vent or a different mounting orientation solves it; other times you'll need to derate the actuator or add a small heat spreader.
Finally, keep documentation honest. The moment you mix a custom actuator with a stock housing, the original IP rating and structural ratings no longer apply as stated. Your own testing becomes the only reliable reference, so note what changed—whether it's a modified end cap, a new seal groove, or just longer screws. That record will save you a lot of confusion later, especially when someone else has to service the unit.
Plating Choices That Survive Harsh Environments
Electroless nickel plating with a high phosphorus content (10–13%) remains a workhorse where salt spray and acidic fumes eat away lesser finishes. Its amorphous, non-crystalline structure leaves no grain boundaries for corrosive agents to exploit, and the coating builds evenly over threads and blind holes. In offshore equipment and chemical processing hardware, 25–50 microns of this alloy often outlasts conventional electrolytic nickel by a factor of two or more.
Hard chrome earns its keep when sliding wear and abrasion dominate, but its micro-crack network can invite pitting unless sealed or paired with a nickel underlayer. For rotating shafts and hydraulic rods exposed to both grit and moisture, a duplex approach—thin electroless nickel base, then hard chrome—strikes a better balance. Alternatively, zinc-nickel electroplate with 12–15% nickel delivers sacrificial protection on fasteners and chassis components, corroding preferentially while the steel stays intact.
Where temperatures swing beyond 400°C or aggressive solvents come into play, ceramic-filled composite coatings or plasma-sprayed alumina show clear advantages over metallic plates. Anodized aluminum with hot-water or nickel-acetate sealing handles marine atmospheres well, though a chromate conversion coat underneath can extend edge retention. Regardless of the chosen chemistry, substrate preparation and post-plate hydrogen embrittlement baking often determine whether a part survives its first season or its fifth.
Small Batches, Big Expectations for OEM Orders
OEM buyers increasingly request smaller production runs, yet they still hold suppliers to standards shaped by mass manufacturing. This creates a tension that many factories struggle to manage: short setup times, frequent line changeovers, and tighter material planning all have to coexist with rigorous quality checks and on-time delivery. The result is a procurement landscape where agility no longer means compromising on tolerances or finish.
For suppliers, the real challenge is not simply producing fewer units. It is recalibrating workflows so that a 500-piece order receives the same attention to detail as a 50,000-piece run. That means rethinking fixture design, inspection frequency, and packaging formats without inflating unit costs. Buyers, in turn, expect clear communication about lead times, component availability, and any deviations before they become delays. A supplier that handles low-volume OEM work well often builds stronger long-term partnerships than one optimized only for high-volume output.
When a Global Brand Needs a Switch That Doesn't Exist Yet
A global brand rarely settles for off-the-shelf parts. When their next product hinges on a switch with a unique feel, unusual footprint, or a custom actuation force, the standard catalogs fall short. The need is precise: a component that does not exist in any distributor's inventory, yet must perform flawlessly from the first prototype to the millionth unit.
This is where the real engineering begins. The brand's team sketches a concept—maybe it's a low-profile rocker that snaps with a particular acoustic signature, or a sealed tactile dome that survives ten million cycles in a dusty environment. Every spec is negotiable except the outcome. Suppliers are asked to step far beyond their existing line cards.
The collaboration becomes a quiet race. Tooling is cut while the switch is still being refined, materials are tested under abuse that goes beyond published ratings, and the final design carries no part number because it was never meant to be a standard product. That switch, born from a blank page, quietly enables the next flagship device.
Testing Every Unit Before It Leaves the Floor
On the final stretch of the assembly line, each unit gets pulled aside for a quick but deliberate pass through a test rig that checks every critical function. No sampling, no spot checks—every single device is powered up, cycled through its diagnostic routine, and watched for any sign of hesitation. The test operator has a laminated checklist with specific voltage readings, timing windows, and connector mating cycles, and they note the results on a paper traveler that follows the unit to the shipping dock. If a unit throws a code or drifts outside tolerance, it is set on a red cart for rework before the next shift starts.
This kind of full-population testing catches the odd failures that batch sampling would miss—a cold solder joint on one board, a batch of capacitors that only misbehave above 40°C, or a firmware flag that flips only after the third power cycle. The test data gets logged against each serial number, so when a field return comes back two months later, the tech can pull up exactly which tests that unit passed and which operator ran them. That traceability has already shortened root-cause investigations from days to a couple of hours.
New hires on the floor often push back at first, saying the test step slows down the line. But after a few weeks, they start catching things the automated equipment misses—a slightly loose display bezel that only shows up when you twist the housing, or a power button that feels mushy on one corner. They begin writing their own notes in the margin of the checklist, and pretty soon the test rig gets a small upgrade: a fixture arm that holds the unit at the exact angle where that intermittent connector fault likes to appear. Testing every unit isn’t just a gate; it turns into a shared habit of looking harder.
FAQ
We produce a broad range, including surface mount, through-hole, right-angle, low-profile, and miniaturized variants. Each series can be adapted with different position counts, actuator styles, and pin configurations to suit the client's product requirements.
Yes. Our engineering team works directly with brand engineers to develop custom contact layouts, sealed housings, or unique actuator colors. We follow a structured DFM process so the custom design moves from 3D model to prototype quickly without compromising reliability.
Our production lines are certified to ISO 9001 and IATF 16949 for automotive-grade components. Each batch undergoes automated inspection for contact resistance, insulation resistance, and actuation force before it ships.
We use automated assembly and vision inspection systems. Critical contact surfaces are plated in-house, and we maintain statistical process control on every line. That means the 100,000th switch performs just like the first one.
Contacts are typically phosphor bronze or beryllium copper with gold or tin plating, depending on the application. Housings are made from high-temperature thermoplastics like PPS or LCP, which survive reflow soldering without warping.
We offer pre-production samples for approval. Prototypes are usually shipped within 10 business days after design freeze. We can also provide small pilot runs so your team can validate the feel, detent torque, and electrical performance in the actual device.
Our rotary dip switches are used in industrial controls, HVAC systems, security panels, automotive electronics, and medical devices. We have experience meeting the strict durability and environmental requirements of each sector.
Conclusion
Inside this OEM rotary DIP switch factory, the calibration room sets the tone: every click is measured for actuation force, travel, and tactile feedback, with readings logged against tolerances tighter than most datasheets admit. Mixing custom actuators with off-the-shelf housings lets the plant answer short-run OEM orders without tooling delays, while a range of plating choices—from gold over nickel to hard gold and tin—ensures switches survive salt spray, humidity, and industrial solvents. Small batches are not an afterthought; dedicated assembly cells and fixture changes happen in minutes, so a run of 500 gets the same scrutiny as 50,000.
When a global brand needs a switch that doesn't exist yet, the engineering team turns a rough sketch into a working sample within days, iterating on detent profile, shaft height, and terminal style until the feel is right. Before anything leaves the floor, every unit is tested for contact resistance, insulation resistance, and cycle life, with serial numbers tied to test data for traceability. That combination of measurement discipline, material flexibility, and per-unit verification is what keeps OEMs coming back for components that carry their name into the field.
Contact Us
Contact Person: Anna lin
Email: [email protected]
Tel/WhatsApp: +86 13567768885
Website: https://www.kjele.com/