Optical Comparator Supplier How to Choose the Right One for Precision Measurement
2026-09-24
Choosing the right optical comparator supplier can make or break your precision measurement workflow. From ensuring micron-level accuracy to navigating after-sales support, the decision is rarely straightforward. But what if the search doesn’t have to feel like guesswork? In this guide, we’ll break down the key factors that separate a dependable partner from a risky bet — and show why many quality-driven teams are turning to JATEN for confidence at every inspection.
Your Tolerances Come First, Not the Supplier’s Feature List
When a drawing lands on a supplier's desk, the first thing they often do is scan for familiar features—thread sizes, surface finishes, maybe a heat treat callout. But for the buyer, what actually keeps a part from failing in the field is rarely the headline spec. It's the tolerance stack-up nobody wants to talk about.
Suppliers love to lead with what they already have in stock or what their machines are set up to run. That's understandable, but it's backward. If you let the conversation start from their capability list, you'll end up compromising on the ±0.005 mm that your assembly actually needs, because it doesn't appear on their feature sheet.
Try this instead: open every sourcing discussion with your tolerance requirements—every one of them, including the ones buried in the notes. Then ask what they can do. A good shop will either confirm the process or tell you exactly where the risk is. The mediocre ones will change the subject back to their standard offering, and that's your signal to walk.
The Lens and Lighting Matter More Than the Spec Sheet
Most people obsess over megapixels and sensor size, but a mediocre lens will soften every single one of those pixels before the file ever reaches your card. A sharp, well-corrected prime wide open shows you texture and micro-contrast that a cheap zoom simply cannot resolve, regardless of the camera body behind it.
Lighting shapes the image far more than any high-ISO claim. A single well-placed softbox can make a bland face interesting, while harsh top light will ruin skin tones on even the most expensive sensor. Learning to shape and control light turns a flat snapshot into a deliberate photograph.
When budget forces a choice, put your money into glass and grip gear before chasing the newest body. A ten-year-old camera with a great lens and a simple off-camera flash will produce more compelling work than the latest flagship with a kit zoom and no light control.
Software Should Bend to Your Workflow, Not Break It
Most software demands that you learn its rules—where to click, what to memorize, how to structure your day around its limitations. But the best tools fade into the background, adapting to the way you already think and work. Instead of forcing you into rigid categories or multi-step menus, they let you rearrange, rename, and reshape the interface until it feels like an extension of your own habits.
This principle matters because workflows are personal. One person might start every morning with a quick capture of loose thoughts, while another needs to review a shared dashboard before touching anything else. Software that bends to your workflow doesn't ask you to abandon those rituals—it offers shortcuts, custom views, and flexible triggers that fit around them. The result is less friction, fewer workarounds, and more mental energy for the actual task at hand.
When a tool breaks your workflow, you notice it immediately: an extra export step here, a rigid tagging system there. But when software bends properly, it's almost invisible. That quietness is the real sign of good design—not a flashy feature list, but the feeling that the tool simply gets out of your way and lets you do your best work.
Insist on a Demo with Your Own Parts, Not Theirs
A vendor's sample parts always look perfect—that's the point. Their pre-polished fixtures, carefully chosen tolerances, and rehearsed cycle times won't reveal how the machine handles your actual workpieces, with all their burrs, variation, and awkward clamping surfaces. When you bring your own parts, the real behavior comes out: chatter on thin walls, slow tool changes between mixed batches, or a spindle that hesitates under your specific load. You're not buying a demo; you're buying capability for your production floor.
Ask the vendor to run a batch of your parts while you watch, from setup to final measurement. Pay attention to how much manual intervention creeps in—does the operator need to babysit a tricky fixture or tweak offsets every few cycles? An honest demo with your components will reveal the gap between a shiny showroom run and what actually happens at 2 a.m. when nobody's adjusting the feed rate. If they resist using your parts, treat that reluctance as the first piece of information about how the partnership will go.
Calibration Claims Mean Nothing Without Traceable Proof
A calibration sticker or a verbal assurance means very little on its own. Anyone can print a label or repeat a phrase. What matters is whether the calibration can be followed back through a documented chain to a recognized standard. Without that chain, there is no way to verify the numbers are actually right.
Traceable proof usually comes in the form of a certificate that lists the instrument, the reference standards used, the measurement uncertainties, and the date. It also identifies the laboratory or body responsible. If a vendor cannot provide that document, or if the details are vague, the claim should be treated as unsubstantiated.
In practice, this matters because decisions get made on the back of those measurements. A drift or error that goes unnoticed because a calibration was never properly verified can lead to rejected parts, safety risks, or costly rework. Demanding traceable evidence is not bureaucracy; it is basic accountability.
After the Sale: Training, Maintenance, and Upgrade Reality
Most vendors will happily walk you through a polished demo before you sign, but the training they deliver afterward rarely matches that depth. In practice, you might get a two-hour screen share that covers only the most basic workflows, leaving your team to figure out the edge cases on their own. The real cost of that gap shows up weeks later, when people quietly revert to old habits or avoid the tool entirely because nobody ever addressed how it should fit into daily routines.
Maintenance agreements look reassuring on paper, with promised response times and guaranteed uptime percentages. Yet the reality often involves chasing down a support ticket while a critical system sits idle, waiting for a part that has to be shipped from another region. Preventive maintenance is frequently skipped until something breaks, and then the repair bill arrives with line items nobody mentioned during the sales pitch. It is not uncommon to discover that basic upkeep requires a specialized technician you cannot hire locally.
Upgrades are sold as a straightforward path to better performance, but the actual rollout can turn into a project of its own. Compatibility issues with existing hardware or data formats surface only after you have committed, and migrating years of records is seldom a one-click affair. Sometimes the new version strips away features your team relied on, or introduces bugs that were not present before. Staying current stops feeling like an advantage when each update forces you to retrain staff and rebuild workflows you had finally stabilized.
FAQ
Focus on measurable capability, not marketing claims. Ask for a GR&R study on the specific comparator model you're considering, performed at your tolerance range. The supplier should also offer onsite verification with traceable artifacts, and their service team needs to understand thermal compensation if your shop floor varies more than a few degrees.
Request a portfolio of past fixtures for parts similar to yours, not just a CAD screenshot. A capable supplier will walk through clamping strategy, material choice for the fixture, and how they validate repeatability before shipping. If they hesitate to discuss setup time or don't ask about your part's datum structure, keep looking.
Neither is automatically better. A manufacturer gives you direct access to engineering changes and proprietary software updates. A reseller might offer more objective comparisons and faster local service for multiple brands. The deciding factor is whether they stock critical spare parts locally and can provide loaner units during repair.
Ask who performs the calibration, whether it's ISO/IEC 17025 accredited, and what happens between annual calibrations. A good supplier will explain how drift is monitored, offer interim check standards, and give you a documented uncertainty budget for your typical measurement tasks instead of a generic certificate.
Give them a real drawing with a challenging feature, such as a small radius or a thread form, and see how they respond. Do they ask for tolerance, material, and surface finish? Can they suggest the correct lens magnification and lighting method without pushing the most expensive package? Their follow-up questions reveal more than a demo.
Software often matters more than hardware for throughput. Test the interface with your actual operators, not just engineers. Ask if it supports CAD import, offline programming, and one-click reporting to your quality system. If the supplier cannot show a workflow that reduces setup time by at least 30 percent on your part family, it's probably not the right fit.
For precision measurement, response time beats upfront savings. A local supplier can send a technician same-day when a lens gets damaged or the stage needs realignment. A distant supplier might offer a better price, but every day of downtime erases that advantage. Ask for a guaranteed response time in writing, not just a promise.
Watch for vague references to many satisfied customers without specific industries or measurable outcomes. A credible supplier will share case studies with actual tolerance ranges, part names, and cycle time improvements. Also be wary if they avoid discussing limitations of their equipment or cannot name a single application where their comparator was not the best choice.
Conclusion
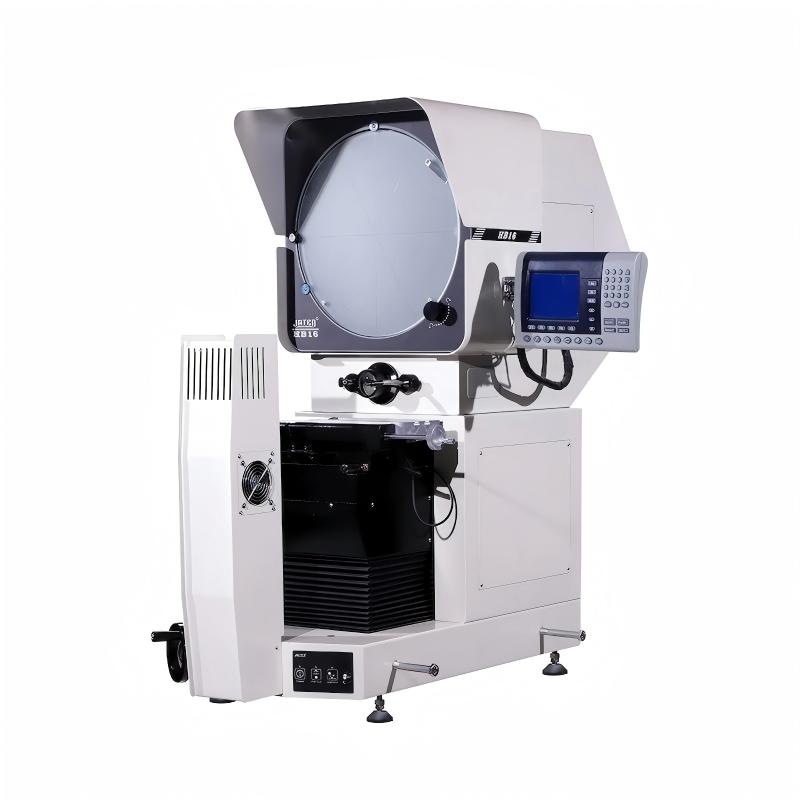
Choosing an optical comparator supplier isn't about who has the longest feature list or the flashiest demo—it's about whether the equipment can actually hold your tolerances on the parts you run every day. Start by defining the measurements that matter to your process, not by comparing spec sheets. A supplier worth your time will ask about your current inspection bottlenecks, your material finishes, and how operators actually use the machine. The lens quality and lighting configuration make a bigger difference in real-world edge detection than any resolution number on paper, so push for a demo using your own difficult parts, not their polished samples. If the image looks fuzzy or the contrast washes out on your worst-case geometry, move on.
Software is where too many precision shops get burned. It should adapt to your existing inspection routines and reporting formats, never force you to rebuild everything from scratch. Ask the supplier to show you how their interface handles your specific GD&T callouts and whether operators can learn it in a day, not a week. Calibration claims are meaningless without traceable documentation—demand certificates tied to NIST or an equivalent national standard, and verify they can recalibrate on-site without shipping the machine back. Finally, dig into the after-sale reality: training depth, spare parts availability, and upgrade paths matter far more than the initial price. A comparator that sits idle because nobody knows how to use it properly is no bargain. Choose a supplier who treats the sale as the start of a long-term measurement partnership, not a one-time transaction.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/