Plywood Die Board Laser Cutting Machine Supplier Guide for Precision Manufacturing
2026-10-04
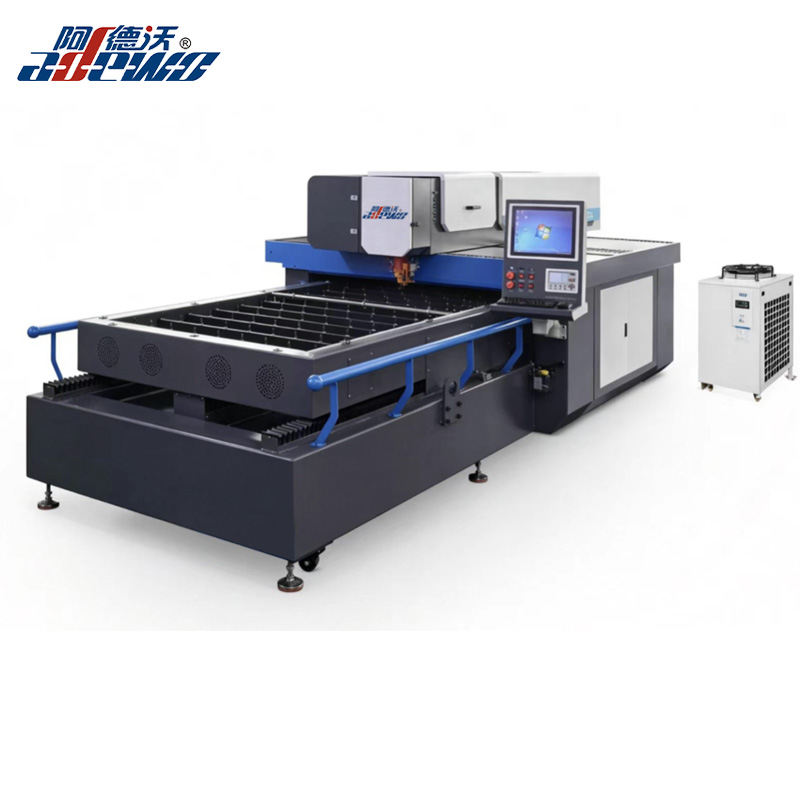
Precision manufacturing demands cutting tools that deliver accuracy without compromise. For plywood die board production, laser cutting has become the go-to method, yet the results hinge on one overlooked factor: the supplier behind the machine. This guide cuts through the noise to show what separates a capable partner from a costly gamble. At the forefront is ADEWO, a name synonymous with robust engineering and tight tolerances. If your next die board run needs to hit spec every single time, the following insights will help you choose with confidence.
Where Laser Precision Meets Plywood Grain
Laser precision meets plywood grain in a way that feels almost unfair to the material. The beam follows a path too fine for any saw, kissing the surface just long enough to vaporize the glue and wood fiber without setting the edges ablaze. On birch ply, the result is a cut so clean you’d swear the sheet grew that way, except the grain still wanders wherever it likes. The contrast between machine exactness and organic swirl is what makes the finished piece feel alive.
You learn quickly that plywood doesn’t bend to the laser’s will without a little negotiation. Resin pockets, uneven veneers, and the occasional knot all shift how the beam bites. Dial in the speed and power too high, and the edge chars into a brittle black line; too low, and you’re left sanding fuzz out of a half-cut groove. The sweet spot sits where the smell of toasted wood just starts to rise, and the cut falls open with a soft tap. That’s where the real craft hides—not in the machine’s specs, but in reading how each sheet answers back.
Reading Supplier Spec Sheets Like a Shop Floor Veteran
Real spec sheets bury critical details in tiny notes or revision blocks, so before trusting the big numbers, scan for callouts that change everything: material condition, heat treatment, plating specs, or a hidden note that overrides the dimension. It's not about reading every line front to back; it's about knowing which lines bite.
On the floor, a tolerance stack or a surface finish symbol can turn a simple part into scrap if you miss the reference datum. Check the title block for revision and date first—if you're holding an old print or spec, the rest is wasted motion. Then cross-check any "unless otherwise specified" defaults against the actual feature.
A veteran also reads between the specs: supplier footnotes about batch acceptance, packaging, or inspection method often matter more than the headline tolerance. Circle anything that affects setup, tooling, or in-process checks, and ignore the marketing fluff about "precision engineered" until the numbers agree.
The Overlooked Link Between Beam Quality and Kerf Consistency
Most laser cutting discussions fixate on raw power, feed rate, and assist gas pressure, yet the spatial characteristics of the beam itself rarely get the same scrutiny. Beam quality, often quantified by the M² factor or beam parameter product, determines how tightly energy can be focused and how uniformly it distributes across the spot. When this quality degrades—even slightly—the focal spot enlarges or develops hot lobes, and the cut front no longer receives a consistent energy density. The result is a kerf that wanders in width, shows uneven taper, or develops micro-irregularities along the edge. Operators may compensate by slowing down or increasing power, but these fixes mask the root cause and often introduce heat-affected zone variability.
The link becomes especially apparent when cutting complex profiles with tight radii or acute angles. A beam with poor quality tends to produce a larger effective spot at the same nominal focus position, which reduces peak intensity and broadens the heat input. Along a straight section, this might still yield an acceptable kerf, but at a corner the additional thermal load causes the kerf to widen unpredictably or the edge to roughen. Because the beam's intensity profile is rarely symmetric once the resonator or fiber delivery drifts out of alignment, the inconsistency is direction-dependent—one side of the cut may show a cleaner edge than the other. This asymmetry cannot be dialed out with standard cutting parameter adjustments, since it stems from the beam's internal structure rather than external process variables.
A practical way to bring beam quality back into the conversation is to correlate kerf consistency with direct beam diagnostics instead of treating them as separate concerns. Measuring M² or capturing the focused spot profile at regular intervals reveals gradual deterioration before it manifests as scrap parts. Simple housekeeping—cleaning protective windows, checking collimation, verifying fiber connector alignment—often yields a more dramatic improvement in edge straightness and kerf repeatability than pushing the laser to higher output. In short, the pursuit of tighter kerf tolerance should start at the beam source and its delivery optics, not just at the cutting head parameters.
Why Fixture Design Decides Your Daily Throughput
The way a fixture locates and clamps a part sets the ceiling on how many cycles you can run before lunch. If operators have to tap a part into place, watch for lift, or reset clamps after every third cycle, those seconds compound across hundreds of parts. A well-thought-out nest with proper datum contact and consistent clamping pressure removes the small hesitations that quietly trap a line at 80 percent of its rated speed.
Changeover time usually tells the sharper story. Fixtures that rely on loose spacers, shims, or tool-specific bolts force a setup technician to make fine adjustments under time pressure. In contrast, a fixture with quick-release locating pins, captured hardware, and pre-set stop positions lets a cell switch from one part number to the next in minutes instead of half a shift. That directly buys back production hours without touching machine feed rates.
Then there is the scrap factor. A fixture that allows slight part rotation under heavy cutting loads may still hold tolerance on the first run, but tool wear and thermal drift gradually push parts toward the edge of the tolerance band. Operators respond by checking more often, slowing feeds, or sorting parts. Getting the clamp points and support locations right on the first design pass avoids that slow bleed of throughput later in the day.
Negotiating the Real Price of Downtime in Die Board Production
When a die board line stops, the visible cost is only the tip of the iceberg. Operators idle, delivery windows slip, and rush orders pile up. But the real price of downtime often hides in places that never appear on a standard production report. Tooling wear accelerates from repeated stops and starts. Adhesive films degrade on half-processed boards. Quality checks get rushed, leading to rework that consumes more hours than the original stoppage. Negotiating that real price means refusing to accept “machine hours lost” as the full story. It demands a line-by-line breakdown of what actually happens during the first ten minutes, the first hour, and the first shift after a breakdown.
The negotiation itself rarely happens in a boardroom. It unfolds on the floor, between maintenance leads, production supervisors, and the scheduler who quietly reshuffles jobs to protect key customers. Each party carries a different assumption about what downtime costs. Maintenance sees a failed drive belt. Production sees 400 sheets of unprocessed die board. Sales sees a late shipment to a client threatening to dual-source. Until those viewpoints are forced onto a single page, the “real price” remains a guess. A practical approach is to audit the last three unplanned stoppages, not by duration, but by consequence. How many boards were scrapped? How much overtime was approved? Which preventive maintenance task was skipped to recover the lost hours? Those answers become the leverage for negotiating better spares inventory, condition monitoring, or even a change in shift overlap.
Die board shops that treat downtime as an accounting problem end up paying for it twice. First in the immediate disruption, then in the hidden costs that surface weeks later as warranty claims, tooling replacements, or exhausted staff. Negotiating the real price requires a recurring conversation, not a one-time analysis. It means agreeing on a common downtime cost model before the next failure occurs. When a line goes dark, the team should already know which metrics they will review and who owns each corrective action. Otherwise, the negotiation happens under stress, with emotions high and data thin. The goal is not to eliminate downtime entirely—that is unrealistic. The goal is to make the true cost visible enough that every hour of prevention is weighed against the genuine, negotiated cost of letting the line stop.
When Automation Claims Collide with Actual Workflow
When a software demo promises automatic routing, it’s usually built on a tidy flowchart. The actual workflow, though, is rarely that neat. People forward things with sticky notes, wait on verbal approvals, or make exceptions for a key client. The automation doesn’t know about those informal rules, so it tries to force every case through the same narrow pipe.
The gap becomes obvious the first time something unusual happens. A purchase order lacks a cost center, or a support ticket mentions two different issues. The system either stops or asks for data no one has. Teams quickly fall back to email and spreadsheets, which means the official workflow and the real one start drifting further apart. Every claim of reduced manual effort gets undercut by the work needed to keep the automation from derailing.
A better approach is to treat the workflow as it actually operates, not as it was documented years ago. Spend time watching where decisions get made, where bottlenecks appear, and which steps people quietly skip. Build automation that can flag exceptions and route them to a person instead of pretending they’ll never happen. Otherwise the tool ends up as another layer of friction, and the promised time savings evaporate in status meetings.
FAQ
Focus on beam quality and motion control. A stable CO2 source with low divergence keeps kerf width consistent, and a gantry with minimal backlash prevents drift on long cuts. Ask for actual test cuts on 15-18mm plywood, not just spec sheets.
Request a list of recent clients in die board production and call one or two. Ask about response times for software issues and spare parts availability. A supplier who cannot name a local technician or keep common lenses and nozzles in stock will cost you more later than the machine price difference.
For plywood die boards, CO2 usually wins because wood absorbs the longer wavelength more efficiently, giving cleaner edges with less charring. Fiber can cut faster on thin material but often leaves more heat discoloration and struggles with thicker plywood unless you add oxygen assist, which complicates the process.
They compare watts per dollar and ignore the cutting bed flatness, extraction design, and software workflow. A machine with poor fume extraction will coat the lens and rails with resin within weeks, and clunky nesting software adds hours to every job. Ask for a full day trial with your own files.
You can find small 1300x900mm machines around 18,000 to 30,000 US dollars, but for production-grade with a 1500x3000mm bed, autofocus, and servo drives, expect 45,000 to 80,000. Beware of prices under 12,000; the tube, lens, and linear rails will likely be replaced within a year.
Ask for the positioning repeatability spec, but more importantly, request a cutting test with a 10mm die board and measure the slot width at multiple points. Check if the machine can hold plus or minus 0.05mm on a 2-meter straight line. Also ask about thermal drift compensation. If the supplier does not understand the term, walk away.
Yes, but you will need adjustable parameters. Plywood needs lower frequency and higher air assist to reduce charring, while acrylic benefits from higher speed and less power to avoid melting. A good supplier provides material libraries for the controller and helps you dial in settings, rather than saying it cuts everything.
It depends on your typical die board dimensions. Most standard die boards are 1220x2440mm or 1500x3000mm, so a machine with at least a 1300x2500mm bed prevents you from having to tile or index larger boards. Going bigger than you need adds cost and floor space without improving precision.
Conclusion
When shops start comparing plywood die board laser cutters, the spec sheet rarely tells the whole story. A machine may promise tight tolerances, but actual kerf consistency depends on how the beam holds up across a full sheet of birch or poplar, not just a quick demo piece. Suppliers who understand grain variation and resin pockets will talk about focal length stability and assist gas flow more than raw wattage. Reading the spec sheet like a floor veteran means looking past headline speed numbers and asking for cut samples from the same plywood grade you run daily. Fixture design also gets overlooked until the first shift realizes that a poorly clamped sheet vibrates just enough to turn a clean cut into a rough edge. The best suppliers will walk you through their vacuum bed or pin registration approach and show how it affects repeatability over hundreds of sheets, not just the first few.
Downtime in die board production carries a real cost that rarely appears in the purchase price. A laser tube replacement or mirror alignment might be quoted as a quick service call, but if the supplier does not stock critical parts locally, you could lose two or three days of cutting. Ask about mean time between failures, but more importantly ask how the supplier handles a beam quality drift notice at 2 p.m. on a Wednesday. Automation claims also need to be tested against your actual workflow. A conveyor or auto-loading system that works in a demo cell may stumble when your operators feed warped or imperfectly stacked plywood. Before signing, run a small batch on the supplier's floor with your own material and your own operator. That hour of testing often reveals more than any brochure or polished presentation.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com