Top 10 Chevron Belt Companies in China You Should Know
2026-09-26
Bulk material handling in China is no longer about just any conveyor belt—it’s about the right profile, especially when inclines are involved. Chevron belts have become the unsung heroes of mining, quarrying, and grain handling, yet most buyers still don’t know which manufacturers truly deliver. XAN is one name that keeps surfacing in industry talk, but it’s far from the only player worth your attention. Here are the top 10 Chevron belt companies in China you should know, and why their offerings might surprise you.
The Quiet Factories Behind China's Chevron Conveyor Belt Surge
Drive through the industrial outskirts of Baoding or Qingdao and you might miss them entirely: low-slung workshops with faded signage, loading docks half-hidden behind poplar windbreaks. Yet these unremarkable buildings churn out a staggering share of the world's chevron conveyor belts, the v-shaped rubber belts that grip gravel, grain, and coal on inclines across mining and agricultural sites. Inside, the air smells of vulcanized rubber and cutting oil. Workers move between hydraulic presses with the economy of long practice, pressing pattern after pattern into continuous sheets of belt. There's no startup glamour here—just the thrum of extrusion lines and the occasional clatter of a forklift repositioning a steel mandrel. The surge in global demand has pushed many of these family-run plants to run three shifts, their only outward sign of prosperity a steady stream of container trucks queuing at dusk.
What sets these factories apart isn't proprietary machinery but an obsessive focus on repeatability. A chevron belt fails when the rubber cleats delaminate under heat or when the fabric carcass stretches unevenly. The quiet plants have spent years tuning their recipes—not in labs with spectrometers, but through trial batches, returned samples, and long phone calls with quarry foremen in Chile or grain elevator operators in Manitoba. Many still mix their own rubber compounds on-site, blending natural and synthetic rubber with carbon black and sulfur according to handwritten logbooks. The best of them can hold a tensile strength tolerance tighter than what some multinational brands specify, and they do it without fanfare. A single press operator in one such plant I visited could judge the plasticity of a batch by pinching a warm strip between thumb and forefinger, a skill honed over two decades.
The surge hasn't made them rich in the way one might imagine. Margins are thin, and competition from smaller workshops is relentless. What the boom has brought is stability—enough orders to keep veteran employees, enough cash to replace a tired curing bladder, enough confidence to refuse the shoddiest export requests. One manager, who asked not to be named, pointed to a stack of green-painted steel crates ready for shipment to a copper mine in Peru. "They don't know our town's name," he said, "but they know the belt won't slip on a 17-degree incline." That, perhaps, is the whole story: not a leap in technology or a marketing blitz, but a thousand quiet factories quietly proving themselves load by load. The chevron belt surge is less a race than a long, patient grind—and these workshops are built for exactly that.
Where Rubber Compounds and Chevron Patterns Get Their Start
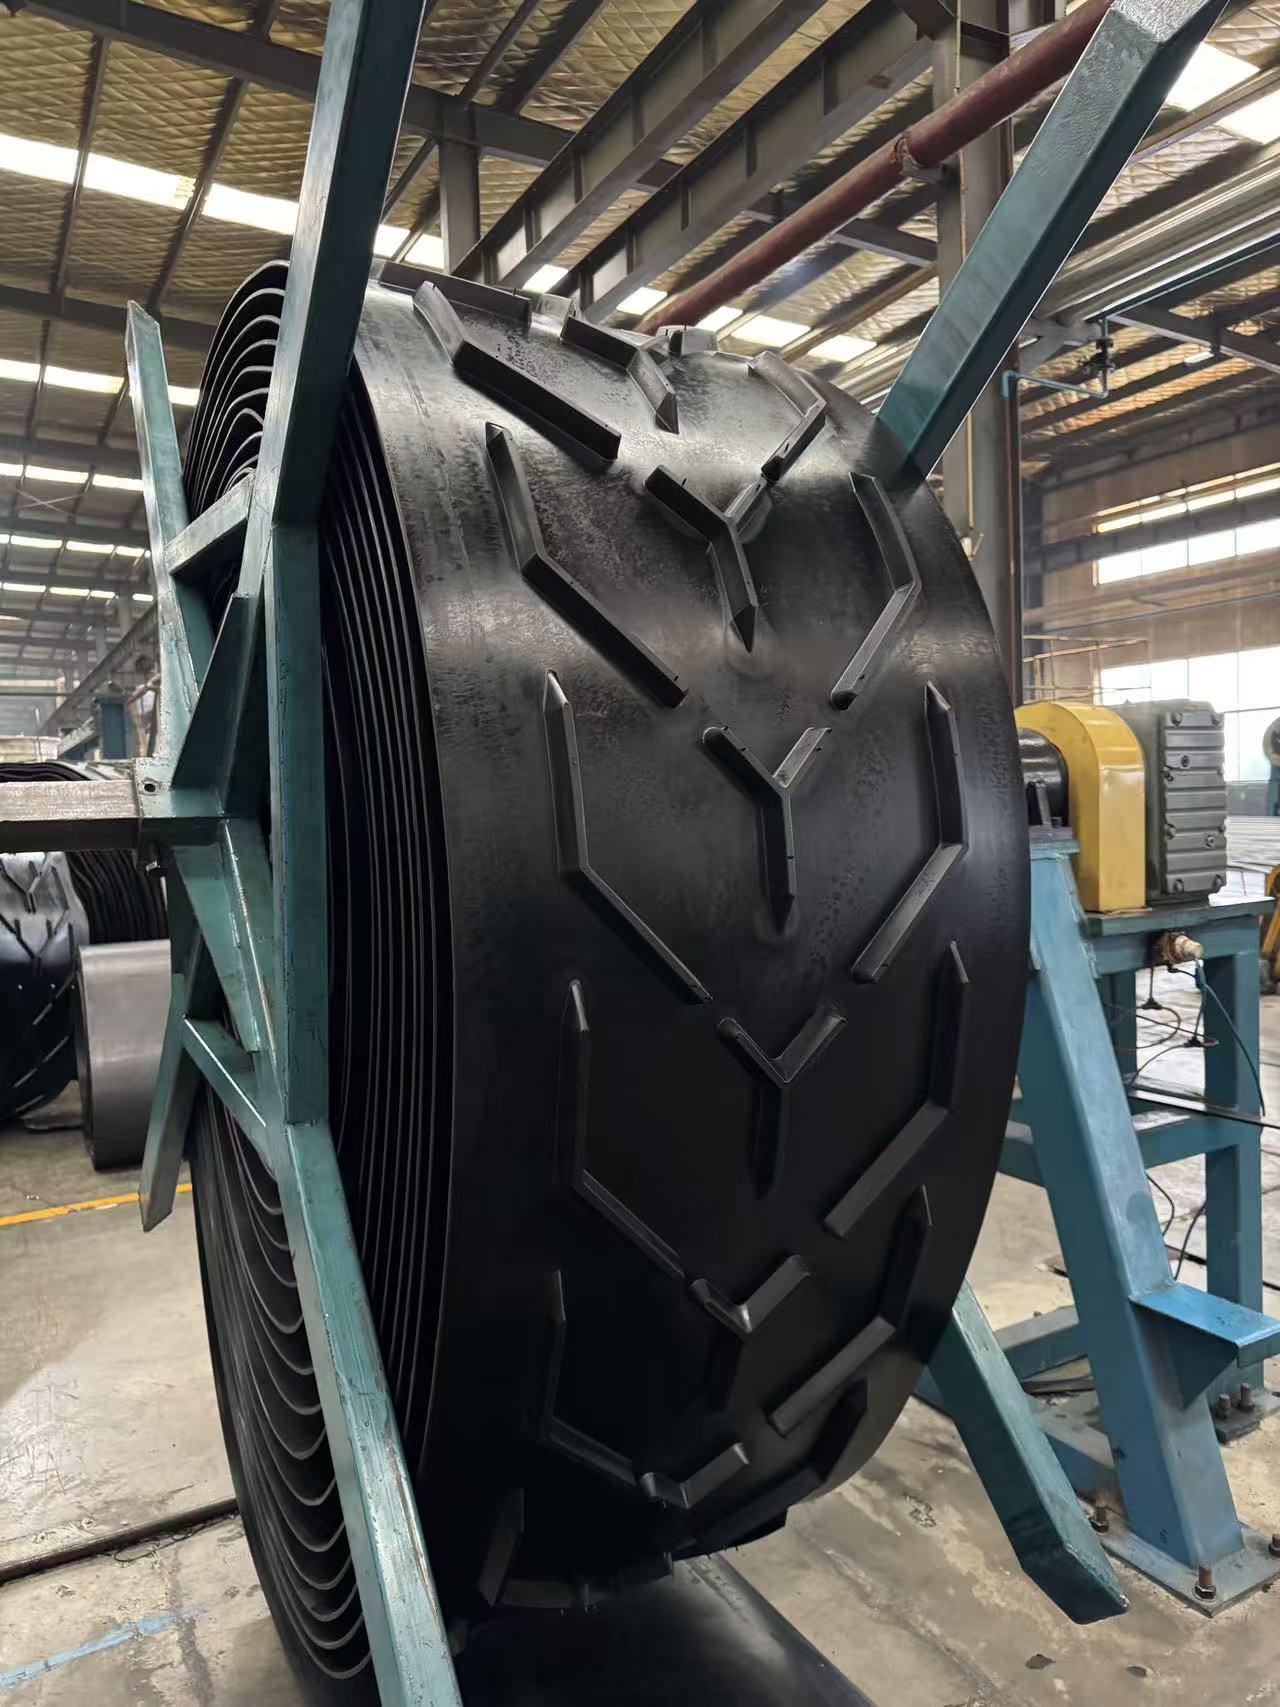
Before a tire ever rolls off the line, its character is set in the mixing room. Raw polymers, carbon black, oils, and curing agents are weighed, dropped into a Banbury mixer, and worked under heat and pressure until they form a uniform slab. The exact ratios and mixing time determine how the rubber will grip, wear, and resist heat later on. Small changes here ripple through every mile the finished product will travel.
Chevron patterns start as a series of hand-drawn sketches and CAD refinements, but the real proof comes from clay models and CNC-cut molds. Engineers study how each lug angle sheds mud, snow, or water, then adjust depth, pitch, and spacing to reduce noise without sacrificing bite. That back-and-forth between digital simulation and physical testing is where a generic tread becomes a recognizable chevron.
Once the compound recipe and tread map are locked, pilot batches are pressed and run through abrasion drums, heat chambers, and wet-track laps. Only after these prototypes meet the target numbers does the design move to production tooling. It is a slow, deliberate start, but one that saves countless hours of rework down the road.
How a Handful of Chinese Manufacturers Set the Durability Bar
Long before durability became a marketing buzzword, a cluster of factories in Shenzhen and Dongguan were already running components through stress tests that most Western brands didn't bother with until warranty claims piled up. Their approach wasn't rooted in premium branding or slick packaging; it came from the brutal economics of export contracts, where a single failed batch could blacklist a supplier for years. That pressure produced an obsession with solder joint integrity, connector mating cycles, and thermal cycling that quietly pushed baseline expectations upward.
What set these manufacturers apart was less about raw materials and more about iteration speed. A hinge that survived 50,000 folds on a prototype would be redesigned within a week to hit 80,000, not because a client demanded it, but because the factory next door already could. This competitive density turned durability from a vague selling point into a measurable, almost tangible benchmark—one that eventually leaked into consumer-facing product lines and reshaped what buyers accepted as normal.
The ripple effect shows up in unglamorous places: longer-lasting USB-C ports, laptop chassis that shrug off drops, power banks that keep full capacity after two years of daily use. These gains didn't come from a single breakthrough. They came from hundreds of small, uncredited decisions made on factory floors, where the cost of failure was always higher than the cost of overbuilding.
Inside the Quality Checks That Separate Long-Lasting Belts From Short-Lived Ones
Most belts fail long before the leather gives out. Stitching unravels, buckles loosen, or the holes stretch into ovals. A handful of workshops still run what amounts to a slow interrogation: flexing the strap thousands of times, yanking the buckle against a deadweight, and soaking samples in salt water to watch for cracking. These aren't lab theatrics. They're the only reliable way to separate a belt that survives a decade of daily wear from one that looks identical on day one but falls apart by the second summer.
The real test often happens in a back room, not on a marketing page. A technician will grab a finished belt, loop it around a steel bar, and hang a 50-pound weight from the buckle. Then they twist. Then they pull at an angle. If the keeper slips or the edge paint flakes off in chips, the whole batch gets rejected. It's boring, repetitive work. Which is exactly why so few brands bother. The ones that do tend to have a drawer full of cracked samples and a very short list of suppliers they trust.
What separates the long-lasting belts isn't a secret material or a patented buckle. It's simply that someone, somewhere, checks them like they'll be worn every single day for years. If a belt survives being clamped, soaked, flexed, and yanked before it ever reaches a box, the odds are good it'll survive your belt loops too.
The Regional Clusters That Produce Most of the World's Chevron Belts
When you trace the global supply of chevron belts back to their roots, a handful of industrial corridors dominate the landscape. The Bohai Rim region in northern China, particularly around Baoding and Qingdao, has become the undisputed heavyweight, with dozens of medium-sized rubber factories running continuous vulcanization lines that churn out millions of meters of cleated belting each year. Not far behind, Gujarat in western India has carved out a niche by pairing aggressive pricing with surprisingly consistent compound quality, a balance that smaller buyers in Africa and Southeast Asia find hard to resist.
Europe's contribution is more specialized but no less critical. The Rhine-Ruhr cluster in Germany and the Lombardy belt in northern Italy focus on high-tensile, heat-resistant chevron profiles used in cement plants and steel mills, where a failed belt can halt an entire production line. These facilities rarely compete on volume; instead, they supply engineers who need exact trough angles, precise cleat heights, and rubber compounds that survive abrasive clinker at 150 degrees Celsius.
What ties these clusters together is a shared ecosystem of raw material suppliers, mold makers, and testing labs that no single factory could replicate alone. A startup in Ohio or São Paulo might build a competent chevron belt, but without the surrounding web of carbon black distributors, textile cord treaters, and second-hand calender lines, matching the cost or turnaround time of the Bohai Rim remains a steep climb.
A Practical Way to Shortlist Chinese Suppliers Without Guesswork
Most sourcing guides throw a hundred supplier names at you and call it a day. That's not shortlisting—that's noise. A cleaner approach starts with mapping your product's failure points. For every component, ask what breaks first, what tolerances actually matter, and which surface finish gets rejected at inspection. Then filter suppliers based on whether their equipment list and past samples show they understand those exact pain points. A factory that has struggled with the same tolerance issue before—and solved it—is worth ten factories with a glossy catalog.
Instead of sending the same generic RFQ to forty vendors, send a short, specific challenge. For example: "We need 10,000 pcs of this bracket, but the bend radius must stay within 0.2mm and the powder coat cannot chip at the mounting holes." Watch how they respond. Good suppliers ask for the print revision, mention a secondary operation, or push back on an unrealistic spec before quoting. Weak ones just quote the lowest price and promise everything. That one round of targeted questions does more real filtering than any audit checklist.
Finally, shortlist by contradiction, not by confirmation. Pick the two suppliers whose quotes and technical answers disagree on something fundamental—like whether anodizing should be done before or after machining, or whether a certain tolerance needs a post-process. Then call both and ask them to explain. The one who can defend their answer with past jobs, photos, and hard numbers is usually the one you keep. The one who gets defensive or vague is off the list. No guesswork needed, just structured pressure on the details that actually affect your product.
FAQ
A chevron belt has raised V-shaped cleats on the top cover, which grip loose material and stop it from sliding back on inclined conveyors. Flat belts often allow material rollback at angles above about 18 degrees, while chevron profiles can be used on slopes up to 30 or 40 degrees depending on cleat height and material.
Coal mines, cement plants, grain depots, port terminals, and sand or aggregate quarries are the main users. Any operation that moves bulk solids up a slope and needs extra grip is likely to choose a chevron belt.
The best Chinese factories use modern mixing lines and multi-stage vulcanizing presses, and their top-end belts can match DIN or RMA standards for tensile strength and abrasion. The main differences are usually price, lead time, and the need for buyers to verify cleat adhesion and compound consistency.
Ask for ISO certificates, request a sample, confirm available cleat heights and rubber grades, and look for a track record in your specific industry. It also helps to check whether the factory exports to demanding markets like Australia or Europe.
Yes, many companies offer open V, closed V, and finger or multi-cleat profiles. Cleat height, pitch, base belt thickness, and cover compound can usually be adjusted to match the incline angle and material weight.
Zhejiang Double Arrow, Baoding Huayue, Shandong Phoebus, Yunnan Shuangjiang, Hebei Yichuan, Wuxi Boton, Qingdao Rubber Six, and Anhui Zhongyi are frequently mentioned in industry sourcing discussions. Each has particular strengths, such as mining belts, port handling, or agricultural profiles.
For standard profiles, 10 to 20 days is common after order confirmation. Custom cleat patterns or special compounds can extend that to 25 to 35 days, and then you need to add shipping time to your destination.
Request third-party abrasion and tensile test reports, ask for reference clients in a similar industry, and if possible arrange a factory audit or send an inspector. A small trial order is also a practical way to check cleat bonding and cover wear under real conditions.
Conclusion
China's chevron conveyor belt industry has quietly built a reputation on precision-mixed rubber compounds and rigorously controlled vulcanization, rather than flashy branding. The factories that matter most aren't the ones with the largest showrooms; they're the ones where raw polymer batches are tested for abrasion resistance before a single mold is filled, and where chevron heights are measured to the millimeter. A handful of manufacturers—often clustered in Hebei, Shandong, and Zhejiang—have set the durability bar by rejecting belts that show even slight delamination under load. Their production floors are less about speed and more about repeatability: the same chevron angle, the same carcass tension, the same cure time, batch after batch.
These regional clusters now supply a staggering share of the world's chevron belts, yet quality varies sharply between plants that invest in in-house tensile testing and those that outsource every check. Savvy buyers shortlist suppliers not by glossy catalogs but by walking through the testing lab: look for evidence of ozone aging chambers, dynamic fatigue rigs, and documented tear-strength curves. The most reliable Chinese manufacturers treat a failed quality audit as a production stoppage, not a negotiation point. If you know which ten companies routinely pass those audits—often the ones that have supplied mining and aggregate operations across Southeast Asia and Africa for over a decade—you can skip the guesswork entirely. The real differentiator isn't price per meter; it's whether the belt still holds its chevron profile after 50,000 cycles of abrasive bulk material.
Contact Us
Contact Person: Anna Lu
Email: [email protected]
Tel/WhatsApp: 8618561668850
Website: https://www.x-conveyor.com