Top Hybrid Servo Press Brake Models for Precision Metal Forming
2026-10-04
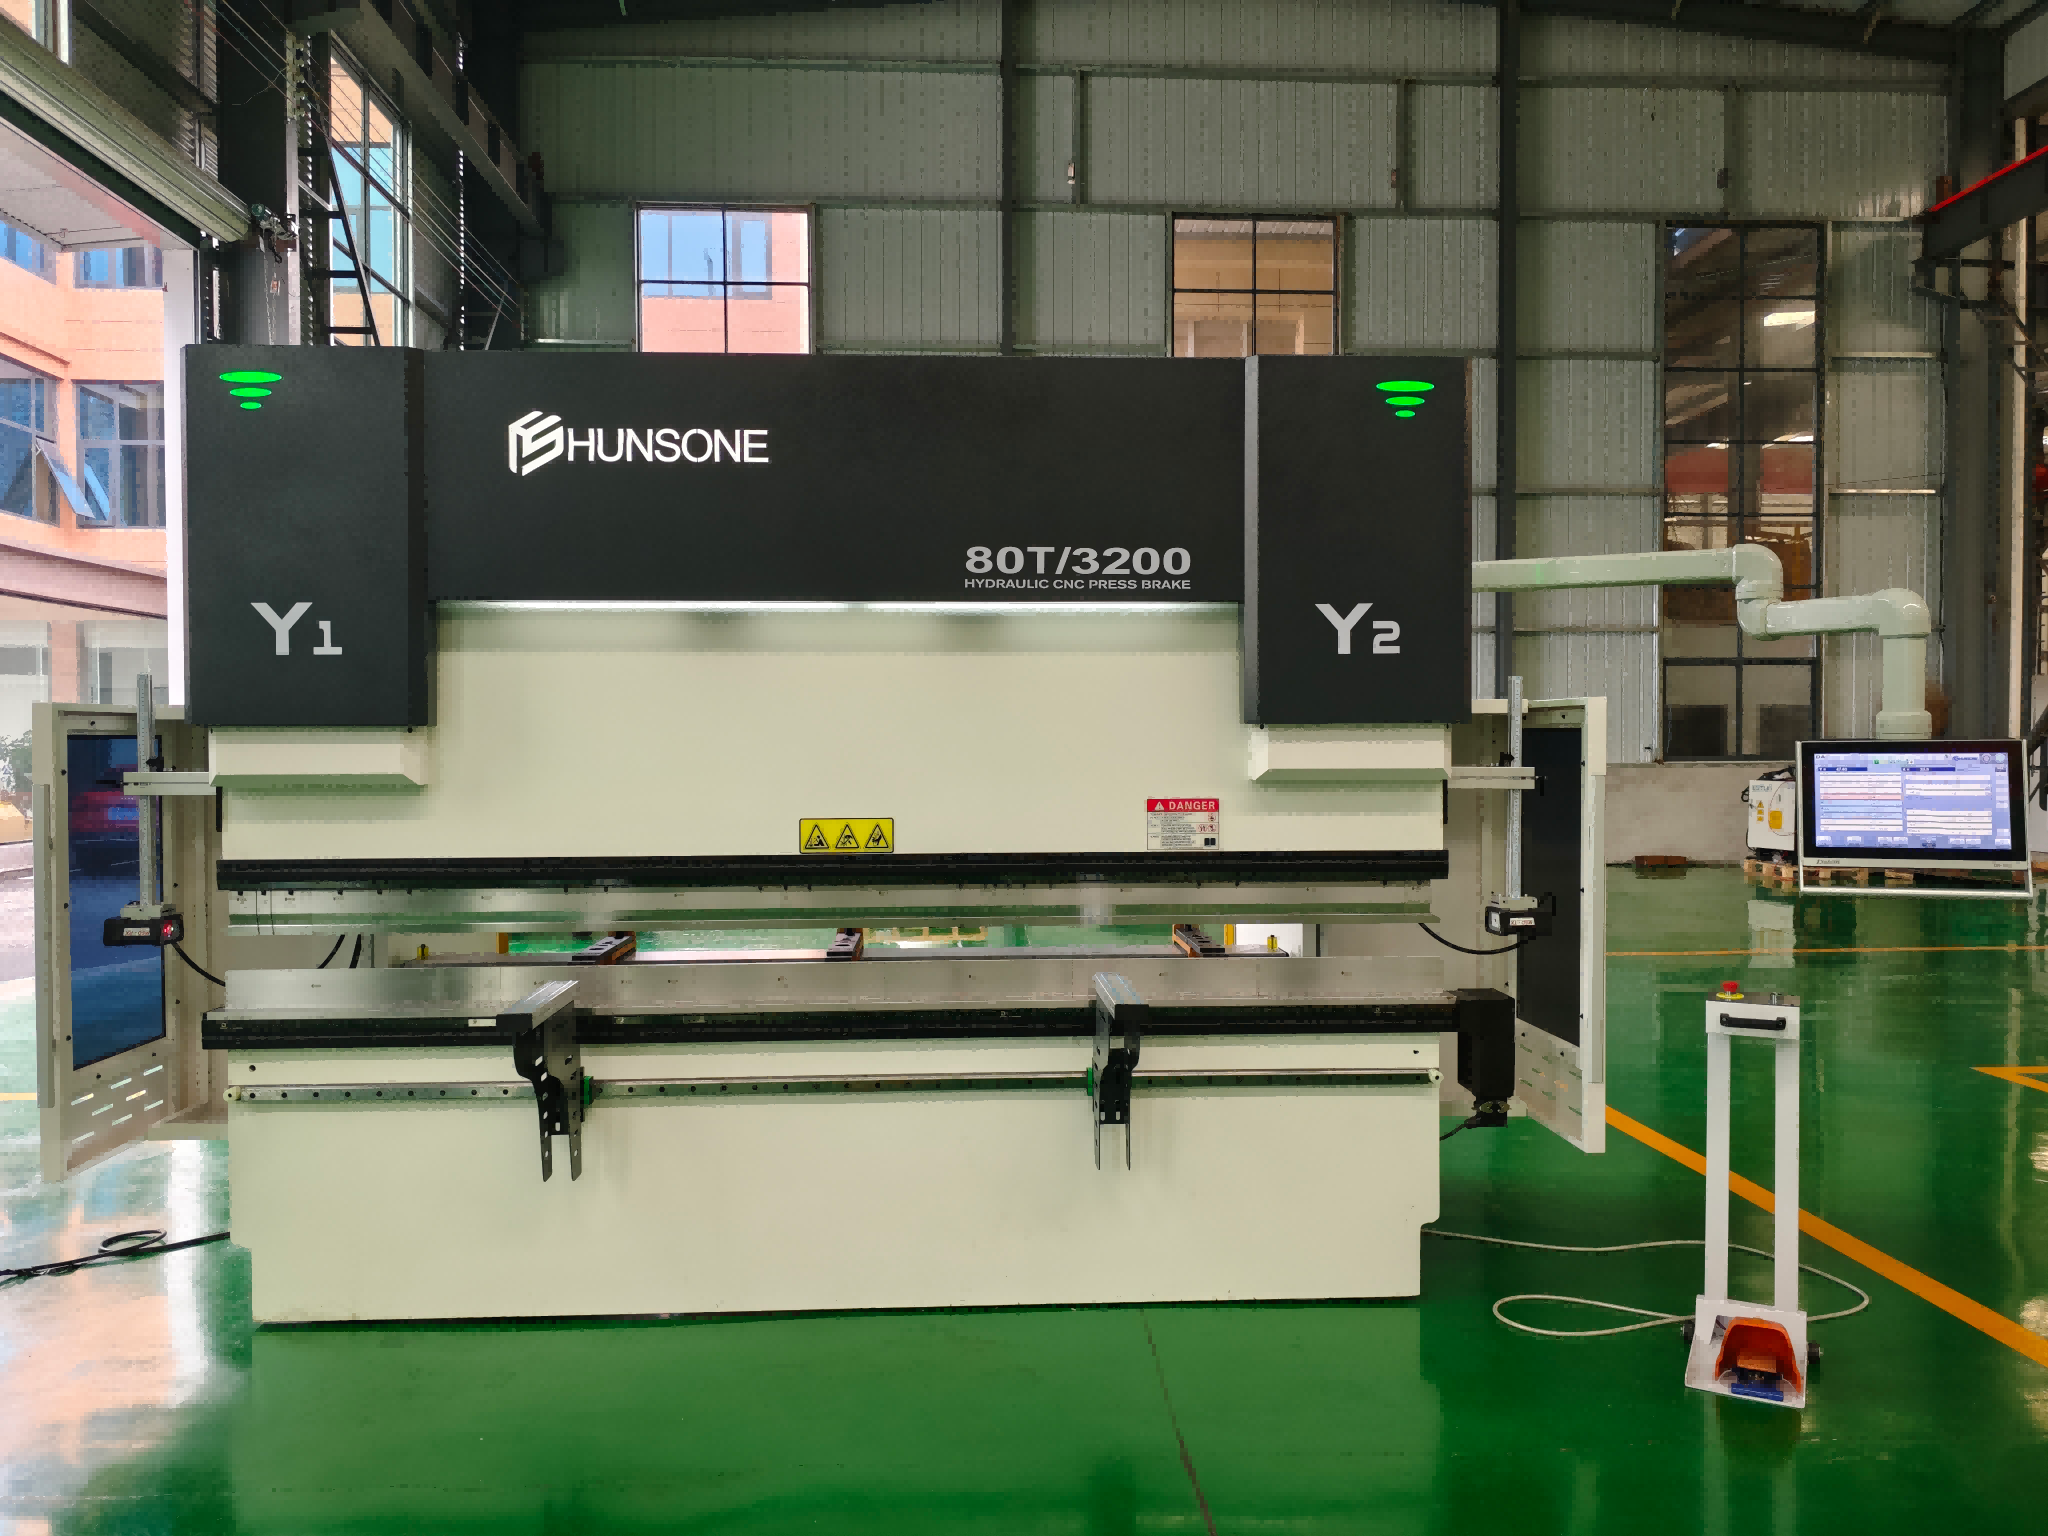
Ask any sheet metal shop about their biggest forming headache, and angle consistency on tricky materials usually tops the list. Hydraulic machines drift, mechanical ones lack flexibility—but hybrid servo press brakes have quietly closed that gap. If you're chasing repeatable precision without sacrificing speed, the right model matters more than the spec sheet suggests. At HUNSONE, we've tested the top contenders so you don't have to. Here are the hybrid servo press brakes worth your attention.
What Actually Separates Hybrid Servo Models on the Shop Floor
The real split between hybrid servo models rarely shows up in spec sheets. On the floor, it’s the behavior under partial load and rapid short-stroke reversals that exposes the differences. Some units hold position with a faint hiss of correction, while others hunt audibly, wasting energy and heating the windings. The good ones blend the holding torque of a stepper with the closed-loop feedback of a servo so smoothly that operators stop thinking about axis drift altogether.
Maintenance access is another separator. A hybrid that mounts its encoder behind a sealed bearing and routes the cable through the same strain relief as the power leads will fail less often than one with a fragile external disk. Shops that run lights-out quickly learn which models tolerate thermal cycling without losing their home offset. The best designs let you swap a motor in under fifteen minutes without re-tuning the drive, because the feedback alignment is factory locked and the drive auto-recognizes the new unit.
Integration friction also matters more than peak numbers. A hybrid servo that requires a proprietary tuning dongle or a Windows-only utility will stall a retrofit project on a Linux-based CNC. Conversely, models that expose step-and-direction plus a simple alarm output and accept industry-standard RS-485 for parameter reads tend to get specified again. In real shops, the winning hybrid is the one that behaves predictably when the air pressure drops, the conveyor jams, or a third-shift operator hits E-stop three times in a row.
The Energy Bill Difference Most Spec Sheets Skip
Most spec sheets reduce energy use to a single annual kilowatt-hour figure, but that number comes from a controlled lab test. Real homes rarely match those conditions, so the actual bill impact gets lost.
For example, two refrigerators with the same Energy Star rating can behave very differently in a warm kitchen or when the door gets opened often. One might run its compressor nearly continuously while the other cycles efficiently. Over five years, that gap can add up to hundreds of dollars.
The spec sheet also won't show standby drain from always-on displays, smart features, or defrost cycles. These small draws are invisible in the headline number, but they quietly shape your monthly bill. Checking real-world reviews and measuring with a plug-in meter reveals what the label skipped.
Bending Precision You Can Repeat Without Constant Shimming
Most press brakes force you into a tedious loop of shimming, test bends, and corrective tweaks just to chase a consistent angle. That routine eats up time and rarely holds up across a full production run. This machine breaks that cycle at the source. The ram and bed are machined as a matched set, and the crowning system reacts to load changes in real time, so the tool gap stays uniform from one end to the other without you ever reaching for a stack of shims.
What you notice first is how the same bend angle shows up on the first part, the fiftieth, and the five hundredth. There is no drift that creeps in after lunch or after a coil change. The control couples angle measurement with automatic compensation, meaning the machine adjusts itself while you keep feeding material. Even operators with little press brake experience can hit the target angle straight away, because the precision is built into the hardware, not into the habit of a seasoned hand.
From a workflow standpoint, that removes a hidden bottleneck. You stop wasting stock on trial pieces, you stop pausing to sweep shims off the floor, and you stop second-guessing whether the next part will match the drawing. Instead, the bending process becomes predictable enough to schedule around. Tooling setups get shorter, scrap rates drop, and the person running the machine can focus on part flow rather than constant correction.
Setup Time Killers and the Controls That Eliminate Them
Most shops lose far more time to setup than anyone wants to admit. The usual culprits hide in plain sight: searching for tools that were never returned, hunting down the right program for a repeat job, and waiting for a fixture that still has chips packed in the locating surfaces from the last run. These delays don't show up on a standard job router, so they get treated as normal friction instead of the controllable waste they really are.
The controls that actually work are often boring, which is exactly why they get skipped. A shadow board with outlined tool positions next to the machine removes the search step entirely. Staging kits with all documents, cutting tools, and gauges pulled before the previous job ends turns internal setup into external setup. And a simple five-minute wipe-down sign-off on every fixture keeps one dirty chip from becoming a thirty-minute alignment fight on the next part number.
None of this requires expensive software or a consultant. It requires a supervisor who walks the floor during setups and asks why the spindle isn't turning. The best shops treat setup time reduction as a daily habit, not a kaizen event. When the team starts timing changeovers with a stopwatch instead of guessing, the real killers surface fast, and the controls become obvious to everyone standing at the machine.
A Rundown of Frames and Crowning Systems That Hold Up
The first thing to look at is how a frame spreads load across its surface. Cheap frames often rely on a couple of thin rails and a center support that flexes after a few months. Better designs use welded corner brackets, extra legs in the middle, and a crossbar that runs the full width. That extra steel or hardwood doesn't just stop wobbling—it keeps the whole platform from developing a low spot where you sleep. A frame that twists or creaks usually passes that movement upward, and you feel it as a mattress that seems to lose support.
Crowning systems take a different approach. Instead of just adding more bracing underneath, they build a slight upward curve into the support layer itself. That crown might be as little as half an inch over the center third, but it counteracts the natural compression that happens from repeated use. Over time, a flat foundation settles and creates a dip, while a crowned one starts a touch high and levels out under weight. Pair that with a rigid frame, and you get a setup that holds its shape for years rather than sagging by the first anniversary.
Which Maintenance Costs Stay Hidden Until Year Three
Most car owners budget for oil changes, tire rotations, and maybe brake pads during the first couple of years. But by year three, the factory warranty often expires right around the same time that several maintenance items come due—and none of them are advertised on the sticker price. Things like brake fluid flushes, cabin and engine air filters, and coolant replacement don't show up in the first two service visits, so they catch people off guard when the third-year invoice arrives. Even the owner's manual may bury these items in a footnote, making them easy to overlook until a technician flags them.
Tires are another quiet budget killer. Depending on your mileage and driving style, the original set can wear down to the wear bars right around the 36,000-mile mark—exactly when many basic warranties end. Add a four-wheel alignment and possibly a suspension inspection, and the cost climbs quickly. Some automakers also recommend a transmission fluid service or spark plug replacement at the 36-month or 40,000-mile interval, even on vehicles marketed as low-maintenance. That's why year three feels like a maintenance cliff: the small stuff you've been deferring suddenly stacks up.
FAQ
The main difference is how the ram gets its power. A hybrid servo model pairs a servo-driven pump with a hydraulic cylinder, so oil only moves when the ram needs to move. That cuts heat buildup, reduces energy draw, and lets the control system hold the ram position far more accurately. On thin stainless or aluminum, you notice the repeatability almost immediately because the servo loop corrects position in real time instead of relying on valve timing.
For intricate work, a mid-tonnage machine around 50 to 80 tons with a short bed—say 1.5 to 2 meters—usually gives the best balance. The shorter bed means less deflection, and the servo control can make very fine ram adjustments. Look for models with a high-speed backgauge and a crowning system, since those two features matter more than raw tonnage when you are chasing tight angles on small brackets.
They are measurable. Because the servo pump only runs when the ram moves, standby power drops dramatically—often by 50 percent or more compared to a constant-running hydraulic pump. Over a year, a busy shop can save several thousand kilowatt-hours per machine. The bonus is lower oil temperature, which means the machine holds calibration longer across a shift and you spend less time on thermal drift compensation.
Look hard at the crowning system and the backgauge stiffness. A good automatic crowning table compensates for deflection under load, which is what actually determines angle consistency. Also ask about the control system's ability to store and recall bend sequences, the speed of the backgauge axes, and how easy it is to program off-line. Those details separate a precision tool from a basic bender.
Yes, if it has a real-time angle correction system. Some top models use sensors that measure the bend angle during the stroke and feed that back to the ram, adjusting on the fly. For high-strength steel, springback varies a lot, so that closed-loop correction is far more reliable than trying to pre-calculate the exact depth. For aluminum, the servo's smooth ram motion helps avoid surface marking from jerky hydraulic starts.
The best ones integrate the control software with a 3D part model. You import the geometry, the software calculates the bend sequence, tooling stations, and backgauge positions, then simulates the full cycle before touching metal. The servo drives then execute those moves with very little overshoot, so the first-off part often comes out within tolerance. That simulation step is what saves time on parts with return flanges or tight inside radii.
It depends on how much those parts are worth and how often you scrap them. For low mix but high value parts, the extra precision and repeatability can pay for itself quickly by eliminating rework. Even if you only run a few jobs a day, the lower heat generation means the first part after lunch will bend like the first part in the morning, which reduces setup passes and material waste.
Keep the hydraulic oil clean and at the right level, but expect to change it far less often than on a conventional machine because it runs cooler. Check the backgauge linear guides for wear and keep them lubricated. Calibrate the crowning system and ram position sensors at least once a year, or more often if you run high-tonnage jobs. Most accuracy problems come from neglected guides or a dirty oil filter, not from the servo drive itself.
Conclusion
Hybrid servo press brakes earn their place on precision metal forming floors through a mix of control logic and mechanical restraint that goes well beyond the motor type. What actually separates them in day-to-day work is how the pump only runs on demand, so the machine isn't burning full power while an operator checks a flange length or rotates a part. This idle-time efficiency shows up as a lower energy bill, but that difference is rarely printed on a standard spec sheet. More importantly, the repeatability of bend angle without constant shimming comes from active crowning tied to real-time load sensing, not just a thicker ram. The controls also remove setup bottlenecks by recalling tool geometry, calculating springback, and adjusting stroke depth automatically, which cuts the number of test bends before the first good part.
The frames and crowning systems on the better hybrid models are built to hold that accuracy over a full shift and beyond. A rigid welded frame with segmented die support keeps deflection in check when you're working near the machine's rated tonnage, and the crowning system compensates for the natural belly in the middle of the bed. Hidden maintenance costs usually show up around year three, when cheaper seals, undersized filters, and stressed hydraulic fittings start to demand attention. Top-tier hybrid servo presses often include predictive maintenance prompts for drive temperature, filter pressure drop, and cylinder wear, which helps avoid surprise downtime. In the end, the models worth shortlisting are the ones that make the energy, setup, and repeatability gains visible on the floor, not just in a brochure.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/